Why does PEEK CNC machining cost so much—and when is it worth every dollar?
Getting a PEEK quote back at 10x the aluminum price feels like a punch. You need the heat resistance, the chemical stability, the wear performance—but the sticker shock makes you second-guess the whole project. And the wrong supplier will crack, warp, or chalk-finish parts you can’t afford to scrap.
PEEK CNC machining is worth the cost when parts face aggressive chemicals, high heat above 250°C, tight wear cycles, or metal-replacement demands. For prototypes, seals, valve seats, and robot bushings, machined PEEK beats molding on lead time and tolerance—if the supplier controls stress, tooling, and annealing.
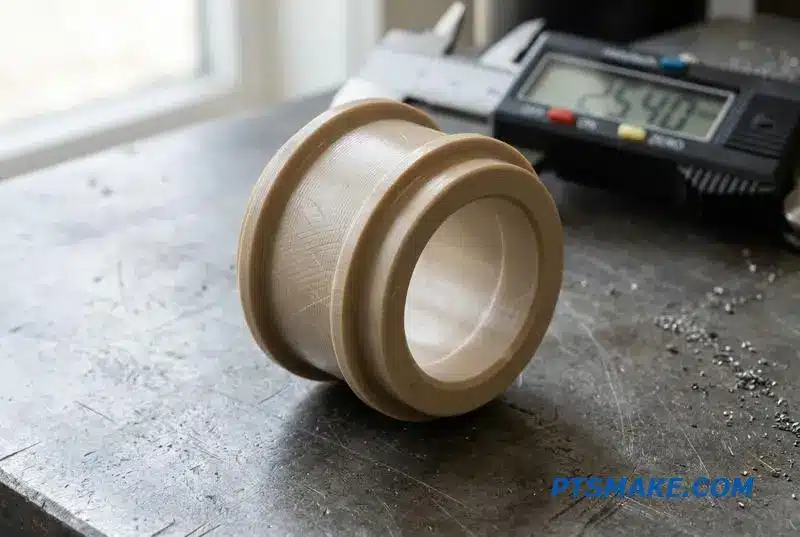
In this guide, I’ll walk you through where PEEK truly earns its price, where cheaper polymers work just as well, and what to ask suppliers so your parts don’t fail on arrival. Let’s dig in.
Why PEEK Parts Cost 10x More Than Their Aluminum Twins
When you compare quotes, the price difference is stark. A PEEK part can easily cost ten times more than its identical twin in 6061 aluminum. This isn’t an arbitrary markup; it reflects fundamental differences in material and manufacturing complexity. The high peek cnc machining cost comes down to a few key factors.
I principali fattori di costo
The primary driver is the raw material. PEEK polymer is significantly more expensive per kilogram than aluminum billet. Secondly, machining PEEK is far more challenging. It requires specialized knowledge and equipment to manage its properties. Lastly, tool wear is much higher, adding to the operational cost.
PEEK vs. Aluminum: Cost Breakdown
| Fattore di costo | PEEK (Polietereterchetone) | Alluminio (6061) |
|---|---|---|
| Costo della materia prima | Molto alto | Basso |
| Lavorabilità | Difficult, requires special care | Easy, well-understood |
| Usura degli utensili | High, abrasive nature | Basso |
| Tempo di ciclo | Slower, requires lower speeds | Veloce |
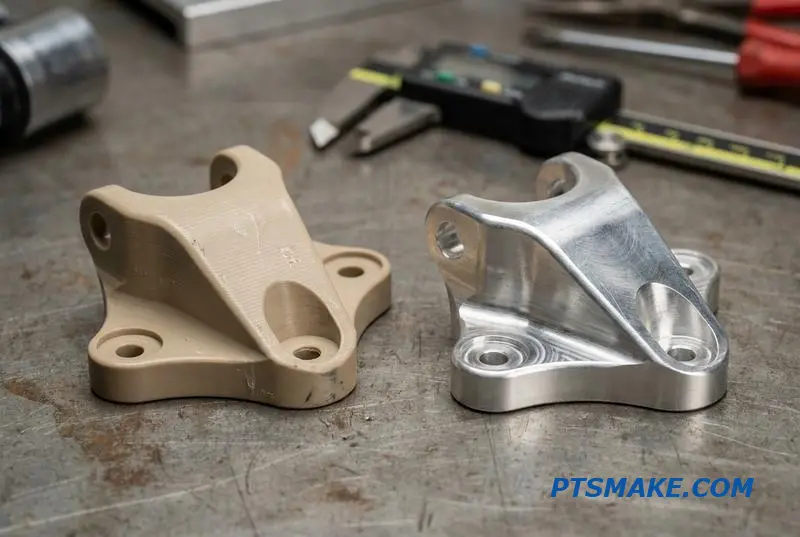
The high price of PEEK is directly linked to its unique properties, which make it challenging to process. Unlike aluminum, PEEK has very low thermal conductivity. This means heat generated during cutting doesn’t dissipate easily through the material. Instead, it concentrates at the tool tip, risking melting the PEEK or damaging the cutting tool.
Specialized Machining Approach
Successful peek cnc machining requires carefully controlled speeds and feeds to prevent heat buildup. It often demands specialized carbide or diamond-coated tools that resist the material’s abrasive nature. A standard high-speed steel tool used for aluminum would dull almost instantly, leading to a poor surface finish and dimensional inaccuracy. This specialized tooling and slower process directly increase the overall part cost.
Waste and Process Control
Furthermore, the high cost of the raw stock means that any scrapped part is a significant financial loss. This demands extremely tight process control and experienced operators. When we machine PEEK at PTSMAKE, we factor in these considerations to ensure every part meets specification without costly errors. The Temperatura di transizione del vetro1 of PEEK also plays a critical role, as machining near this temperature can alter the material’s internal stresses and stability.
The high cost of PEEK parts isn’t arbitrary. It stems from expensive raw materials, challenging machining processes, and increased tool wear. Choosing PEEK is an investment in its superior performance, justified by the application’s demands where aluminum simply cannot perform.
Where PEEK Beats Metal: Seals, Valve Seats, and Bearings
Metals are strong, but not always the best choice. In demanding applications, Polyetheretherketone (PEEK) often provides superior performance. I’ve seen PEEK solve persistent issues where steel or aluminum failed, especially in components that move or seal under stress.
Critical Sealing Applications
For seals and valve seats, PEEK offers excellent chemical resistance and can handle high pressures and temperatures without deforming. This ensures a reliable, long-lasting seal, reducing maintenance needs. PEEK valve seat machining is a core competency for creating these reliable parts.
Bearings and Wear Components
In bearings and bushings, PEEK’s low friction and high wear resistance are key. Unlike metal, it doesn’t require external lubrication in many cases and won’t seize or gall.
| Caratteristica | Componente PEEK | Metal Component (e.g., Bronze) |
|---|---|---|
| Attrito | Inherently low | Requires lubrication |
| Corrosione | Inert to most chemicals | Susceptible to corrosion |
| Peso | Leggero | Significantly heavier |
| Vita utile | Extended in harsh environments | Shorter due to wear/corrosion |
Deciding between PEEK and metal requires a clear look at the operating environment. Metal’s strength is often its main advantage, but that strength comes with trade-offs like weight and a susceptibility to corrosion, which can be critical failure points.
PEEK in Fluid Control and Robotics
In high-pressure fluid control systems, metal valve seats can corrode or wear from abrasive media. PEEK seals and seats solve this. They maintain dimensional stability under pressure and resist aggressive chemicals, ensuring system integrity. This is where precision lavorazione cnc peek really proves its value.
For robotic mechanisms, weight and friction are constant concerns. Using PEEK for bearings, bushings, and wear plates reduces the overall mass. This allows for faster movements and lower energy consumption. The study of friction and wear, or Tribologia2, is central here. PEEK’s self-lubricating properties make it an ideal material for peek bearing cnc applicazioni.
| Applicazione | Common Metal Problem | PEEK Advantage & Operating Condition |
|---|---|---|
| Chemical Pump Valve Seat | Corrosion from acids | Chemical inertness; up to 250°C |
| Robot Arm Bushing | Galling, needs grease | Self-lubricating; high cycle rates |
| Downhole Tool Seal | Failure under pressure/heat | High strength; >150°C, >10,000 psi |
| Wafer Handling Component | Particle generation | Low outgassing; cleanroom compatible |
Choosing PEEK isn’t just about material substitution. It’s a design upgrade for components in challenging environments. The benefits in performance and longevity often justify the switch from traditional metals, especially in precision applications developed at facilities like PTSMAKE.
PEEK is a strategic upgrade for specific high-stress roles. For seals, valve seats, and bearings in harsh environments, its combination of chemical resistance, low friction, and temperature stability delivers performance and longevity that metals often cannot match.
The Fluid-Control Sweet Spot: PEEK in Valves and Manifolds
In fluid control, materials face a constant battle against pressure, temperature, and corrosion. Finding a material that excels across these areas is key. PEEK (Polyetheretherketone) consistently emerges as a top performer for critical valve and manifold components, offering a unique combination of properties.
Why PEEK Excels
PEEK provides a robust alternative to metals and other polymers. Its inherent stability ensures reliable performance in systems where failure is not an option. This makes it a preferred choice for high-stakes applications where precision and durability are paramount.
PEEK vs. Stainless Steel
| Proprietà | SETTIMANA | Acciaio inox 316 |
|---|---|---|
| Peso | Leggero | Pesante |
| Resistenza chimica | Excellent (Broad) | Good (Corrodes with chlorides) |
| Lavorabilità | Buono | Moderato |
| Sealing Ability | Excellent (Conforms well) | Poor (Requires soft seals) |
This balance of properties makes PEEK CNC machining a strategic choice for creating components that optimize fluid control systems.
When we look closer at fluid-control systems, PEEK’s advantages become very clear. Its use in valve bodies, seats, pistons, and insulators is not accidental. The material solves specific problems that plague hydraulic and pneumatic systems handling aggressive media.
PEEK in Demanding Systems
For example, its exceptional chemical resistance makes it ideal for handling corrosive fluids that would degrade metals. Many of my projects involving peek hydraulic valve parts are for systems that process acids, solvents, or high-purity chemicals, where material inertness is non-negotiable.
Resisting Chemical Attack
The material’s ability to withstand chemical degradation is critical. Unlike many plastics, PEEK shows minimal swelling or weakening when exposed to a wide range of substances, even at elevated temperatures. Its resistance to Hydrolysis3 is particularly important in steam or hot water applications.
| Media | Compatibility with PEEK |
|---|---|
| Hydraulic Fluids | Eccellente |
| Sulfuric Acid (Dilute) | Eccellente |
| Sodium Hydroxide | Eccellente |
| Jet Fuel | Eccellente |
Precisione peek valve seat machining is essential because the material’s low friction coefficient ensures a tight seal and smooth actuation, reducing wear over millions of cycles. In peek pneumatic components, its thermal stability prevents deformation under high-pressure, high-temperature air.
PEEK is an optimal material for critical fluid-control components like valves and manifolds. Its superior chemical resistance, thermal stability, and low friction provide reliability and longevity in hydraulic and pneumatic systems, outperforming traditional materials in aggressive environments.
PEEK in Robots: Lightweight Wear Parts That Outlast Plastic
In robotics, wear and tear are constant enemies of uptime. Standard plastics like nylon and acetal often fail in high-cycle applications due to heat buildup and material fatigue. This leads to costly downtime and frequent maintenance cycles, which I’ve seen frustrate many engineering teams.
The Problem with Conventional Plastics
Conventional materials can’t handle the repetitive stress and friction found in modern robotic joints and actuators. They deform under load and lose dimensional stability at elevated operating temperatures. This compromises the robot’s precision and reliability over time, a critical failure point.
PEEK as a Durable Solution
This is where PEEK excels. Its superior mechanical strength and thermal stability make it ideal for demanding components. By upgrading to PEEK for critical wear parts, engineers can significantly extend the operational life of their robotic systems and reduce maintenance schedules.
| Caratteristica | SETTIMANA | POM (acetale) | Nylon 6/6 |
|---|---|---|---|
| Max Service Temp. (°C) | 250 | 90 | 95 |
| Resistenza alla trazione (MPa) | 95 | 65 | 80 |
| Resistenza all'usura | Eccellente | Buono | Fiera |
| Resistenza chimica | Eccellente | Buono | Buono |
When designing robotic systems, material choice directly impacts long-term performance. For components like bushings, gears, and rollers, the debate often centers on PEEK versus more common polymers. While nylon and POM are suitable for lower-demand applications, they can’t match PEEK’s resilience.
High-Cycle Bushings and Gears
In continuous motion systems, heat generated from friction is a major issue. We’ve conducted tests showing that nylon parts in robotic joints can deform after several thousand cycles. A PEEK bushing, however, maintains its integrity well beyond that, thanks to its low wear rate and high heat deflection temperature.
Actuation and Insulator Components
PEEK’s excellent dielectric properties also make it a prime candidate for electrical insulator carriers within motors and actuators. It provides structural support without compromising electrical safety. This dual-purpose capability simplifies design and enhances reliability in compact robotic assemblies, where space and performance are both critical. The material’s low Coefficiente di attrito4 further reduces energy loss in actuation. At PTSMAKE, our experience in PEEK CNC machining ensures these complex parts meet tight tolerances for optimal performance.
PEEK offers superior wear resistance and thermal stability for critical robotic components. This makes it a strategic upgrade over standard plastics like nylon or POM, extending a robot’s operational life and significantly reducing long-term maintenance costs and downtime.
PEEK vs PTFE vs Nylon: Picking the Right High-Performance Plastic
Engineers often default to PEEK for demanding applications, but it’s not always the most practical or cost-effective choice. Understanding the specific strengths of PTFE and Nylon can lead to better design outcomes and significant cost savings. The key is matching the material to the exact operational need.
Confronto tra le proprietà chiave
Choosing the right material involves a trade-off between performance and budget. PEEK offers the highest performance but at a premium price. PTFE and Nylon provide excellent value for specific applications where their unique properties shine.
| Proprietà | SETTIMANA | PTFE | Nylon |
|---|---|---|---|
| Temperatura massima di servizio. | ~250°C (482°F) | ~260°C (500°F) | ~85°C (185°F) |
| Resistenza all'usura | Eccellente | Good (Self-Lubricating) | Molto buono |
| Cost Tier | Alto | Medio | Basso |
Quando scegliere ciascun materiale
SETTIMANA
Select PEEK for components in extreme heat, aggressive chemical environments, or high-load situations. It’s ideal for aerospace, medical, and semiconductor parts.
PTFE
Use PTFE where low friction and chemical inertness are critical. It excels in seals, gaskets, and non-stick surfaces, but not for structural parts.
Nylon
Nylon is a workhorse for mechanical parts like gears, bearings, and bushings due to its toughness and wear resistance at a low cost.
When we move beyond basic properties, the machining differences become critical. In my experience at PTSMAKE, the nuances of lavorazione cnc peek versus working with PTFE or Nylon directly impact project timelines and final part quality. Material choice isn’t just about performance data.
Resistenza chimica e ambientale
PEEK stands out with its exceptional resistance to a broad spectrum of chemicals, steam, and radiation. PTFE is nearly inert, resisting almost all industrial chemicals. Nylon, however, has poor resistance to strong acids and bases and can absorb moisture, which may affect its dimensional stability.
Machinability and Cost Implications
Each material behaves differently on a CNC machine. PEEK is hard and abrasive, requiring specific tooling to manage wear. While stable, the raw material cost is the primary driver of its high price. Good peek vs ptfe machining knowledge is essential to avoid issues like melting.
PTFE is soft and can be challenging to hold tolerances without specialized techniques to prevent deformation. Nylon machines easily, but its tendency to absorb moisture means it must be handled correctly pre-machining to ensure dimensional accuracy. This is a common point of failure in peek vs nylon cnc projects. The material’s Rigidità dielettrica5 is also a key factor in certain electronic applications.
| Fattore | SETTIMANA | PTFE | Nylon |
|---|---|---|---|
| Usura degli utensili | Alto | Basso | Basso |
| Velocità di lavorazione | Moderato | Alto | Alto |
| Stabilità dimensionale | Eccellente | Fiera | Good (If Dry) |
| Costo relativo | $$$$ | $$ | $ |
Choosing the right high-performance plastic is about balancing specific application demands with your budget. While PEEK is a superior all-around material for extreme conditions, PTFE and Nylon offer excellent, cost-effective solutions for applications requiring lubricity or mechanical toughness, respectively.
Why PEEK Stress-Cracks — and How to Design Around It
PEEK is a fantastic material, but it can fail unexpectedly from stress cracking. This issue often traces back to internal stresses locked within the part during manufacturing or due to poor design choices. Understanding the causes is the first step toward prevention.
Key Factors in PEEK Stress Cracking
The most common culprits are sharp internal corners and uneven cooling rates. These factors create stress concentration points where cracks can begin. In our experience with PEEK CNC machining, controlling these variables is critical for part longevity and performance.
| Fattore | Impact on Stress Cracking |
|---|---|
| Velocità di raffreddamento | Fast, uneven cooling locks in stress. |
| Angoli vivi | Concentrates stress, creating weak points. |
| Spessore della parete | Abrupt changes cause differential shrinkage. |
| Ricottura | Relieves internal stress post-machining. |
Proper design and process control are not optional; they are essential for reliable PEEK components.
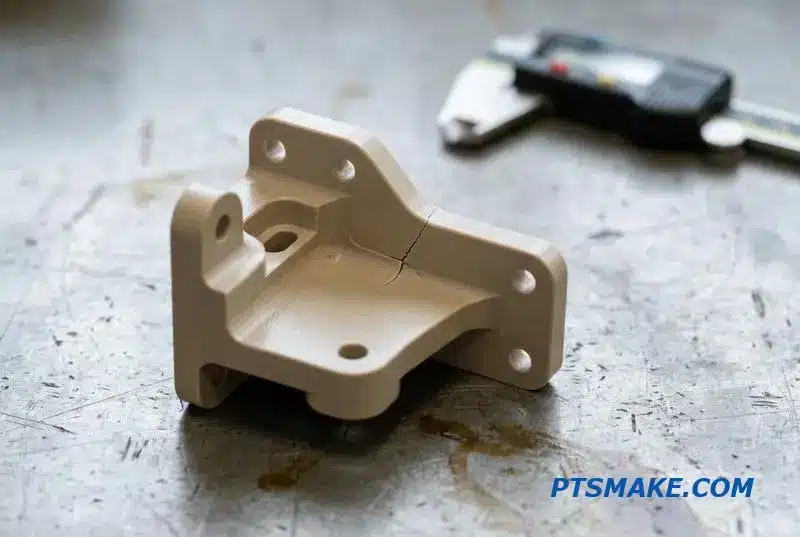
Machining’s Role in Stress Formation
PEEK’s sensitivity to cracking is not just a material property; it’s heavily influenced by the manufacturing process. Every cut made during CNC machining introduces heat and mechanical force. If not managed correctly, this builds up internal Residual stress6, which is the stress remaining in the material after the external forces are removed.
This is why tool selection and cutting parameters are so important. Using sharp tools, appropriate feed rates, and adequate coolant helps minimize the stress induced during machining. At PTSMAKE, we have developed specific protocols for PEEK to ensure part stability.
Design and Process Control Checklist
After machining, an annealing cycle is often the best way to relieve these built-up stresses. It allows the polymer chains to relax into a more stable state. Neglecting this step can lead to premature PEEK part failure, especially in chemically aggressive or high-temperature environments.
| Punto di controllo | Azione raccomandata |
|---|---|
| Raggi interni | Minimum radius of 0.5mm; larger is better. |
| Utensili | Use sharp, new tools specifically for polymers. |
| Raffreddamento | Apply consistent, high-pressure coolant. |
| Ricottura | Perform post-machining stress relief cycle. |
Controlling PEEK stress cracking requires attention to both design and manufacturing. By managing internal radii, wall thickness, and post-machining processes like annealing, we can prevent PEEK part failure. This ensures components perform reliably under demanding conditions.
What Tolerances PEEK Parts Can Actually Hold
When discussing PEEK CNC machining, the first thing to understand is that PEEK is a high-performance polymer, not a metal. This distinction is critical for setting realistic expectations for tolerances. Its properties, especially thermal expansion, dictate what can be consistently achieved.
Grounding Expectations in Reality
Many engineers expect metal-like precision from PEEK. While very tight tolerances are possible, achieving them requires specialized knowledge. The material’s tendency to expand and contract with temperature changes is a primary factor we must manage throughout the machining and inspection process.
Achievable Machining Tolerances
Based on our tests, standard PEEK machining tolerance can be held reliably. For critical features, tighter tolerances are possible but require a controlled environment and specific machining strategies. Below is a general guide.
| Tipo di caratteristica | Tolleranza standard | Tolleranza di precisione |
|---|---|---|
| Diameters/Lengths | ±0,005" (±0,127 mm) | ±0,001" (±0,025 mm) |
| Hole Positions | ±0,003" (±0,076mm) | ±0.002" (±0.050mm) |
| Flatness/Parallelism | 0.002"/inch | 0.001"/inch |
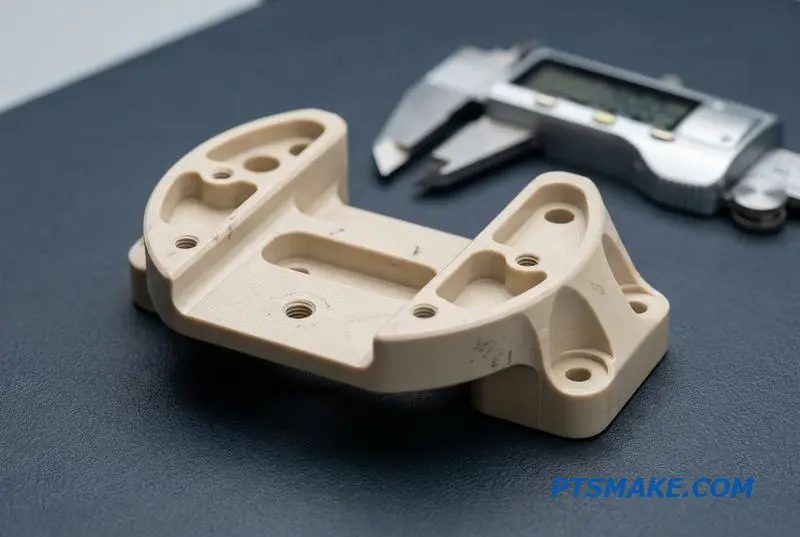
A common issue we see is the mismatch between design specifications and material behavior. PEEK’s dimensional stability is excellent for a polymer, but it still moves more than metals. This becomes evident during inspection, where ambient temperature plays a significant role.
L'impatto dell'espansione termica
Il Coefficiente di espansione termica7 (CTE) for PEEK is much higher than that of steel or aluminum. A part machined at 22°C might measure out of spec if inspected in a room at 25°C. This isn’t a machining error; it’s physics.
| Materiale | CTE (per °C) |
|---|---|
| SETTIMANA | ~55 x 10⁻⁶ |
| Alluminio | ~23 x 10-⁶ |
| Acciaio | ~12 x 10-⁶ |
Ensuring Fair Inspection
To avoid disputes, specify a standard inspection temperature on your drawings, typically 20°C (68°F). This creates a fair and repeatable standard for both the manufacturer and the client. At PTSMAKE, we control our inspection environment to ensure all measurements for plastic CNC tolerance are accurate and reliable. This simple step aligns expectations and guarantees parts function as intended.
Understanding PEEK’s material properties, especially its thermal expansion, is key to successful PEEK CNC machining. Setting realistic tolerances and defining a standard inspection temperature on drawings ensures that parts meet functional requirements without unnecessary complications during quality control.
Why Your PEEK Is Coming Off the Machine Chalky or Stringy
If your PEEK parts have a chalky surface or stringy edges, you’re seeing signs of incorrect machining. These are not just cosmetic flaws. They often indicate that the material’s integrity might be compromised due to excessive heat or improper tool engagement during the PEEK CNC machining process.
Common Visual Defects
A poor surface finish can lead to premature part failure. Understanding the visual cues is the first step in diagnosing the root cause. This helps ensure that the final component meets both aesthetic and functional requirements for demanding applications.
What Causes a Poor PEEK Surface Finish?
The most common issues stem from heat management and tool selection. Dull tools, incorrect speeds, or inadequate feed rates are primary culprits. We can trace each visual defect back to a specific parameter that needs adjustment.
| Difetto | Causa primaria |
|---|---|
| Chalky/White Surface | Dull tooling, excessive heat |
| Stringy Burrs | Low feed rate, incorrect tool geometry |
| Discoloration (Brown/Dark) | High spindle speed, insufficient coolant |
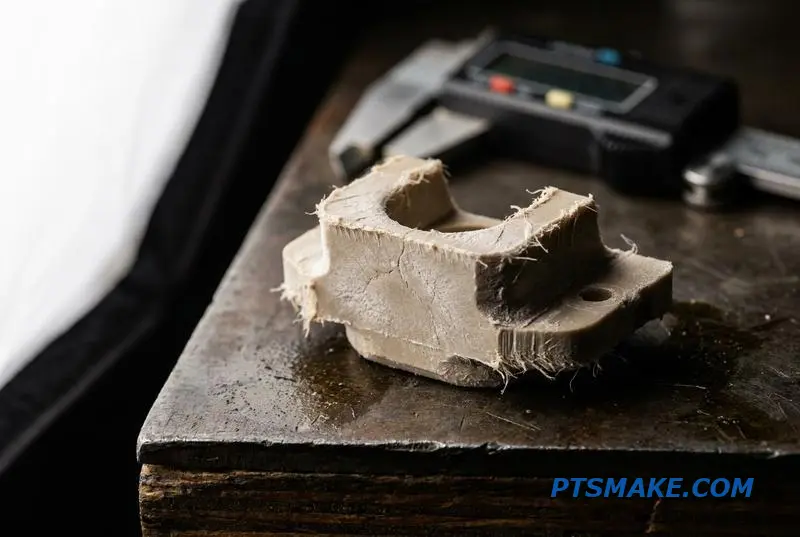
Achieving a high-quality machining peek finish quality on PEEK is about managing heat and chip formation. The goal is to shear the material cleanly, not push or melt it. This requires more than just standard machine settings; it demands a process optimized specifically for this high-performance polymer.
Tooling and Parameter Optimization
At PTSMAKE, we use extremely sharp, uncoated carbide or diamond-coated tools. Sharp edges reduce cutting forces and minimize heat generation. PEEK’s inherent Duttilità8 is why it can produce long, stringy chips if feed rates are too slow. A higher feed rate actually encourages the chip to break cleanly.
Acceptance Criteria for PEEK Components
A well-machined PEEK part is easily identifiable. Based on our experience, proper peek burr removal should be nearly unnecessary if the initial machining is correct. Below are the standards we use to distinguish good work from bad.
| Criteri | Acceptable Standard | Unacceptable Defect |
|---|---|---|
| Finitura superficiale | Smooth, semi-glossy, consistent color | Chalky, white, or discolored patches |
| Qualità dei bordi | Clean, sharp edges with minimal burrs | Stringy, melted, or heavy burrs |
| Precisione dimensionale | Within specified tolerances | Out of tolerance due to heat distortion |
A chalky or stringy finish on PEEK is a direct result of improper tooling and incorrect machining parameters. Achieving a quality peek surface finish cnc requires precise control over heat, tool sharpness, and feed rates to manage the material’s unique properties effectively.
Annealing PEEK: The Step Cheap Suppliers Skip
When you receive a PEEK part that looks perfect but fails later, the cause is often invisible stress. Machining introduces internal stress into PEEK. Without proper treatment, this can lead to warping or cracking over time, especially in demanding applications.
The Hidden Cost of Skipping a Step
Many suppliers skip annealing to lower quotes. This shortcut compromises the long-term integrity of the component. A part that deforms or fails in service is far more costly than one that was properly processed from the start.
Annealing vs. Non-Annealing Outcomes
| Caratteristica | Non-Annealed PEEK | Annealed PEEK |
|---|---|---|
| Stabilità dimensionale | Povero | Eccellente |
| Stress interno | Alto | Minimo |
| Cracking Risk | Alto | Basso |
| Affidabilità a lungo termine | Imprevedibile | Prevedibile |
This simple heat treatment is a critical part of reliable peek cnc machining.
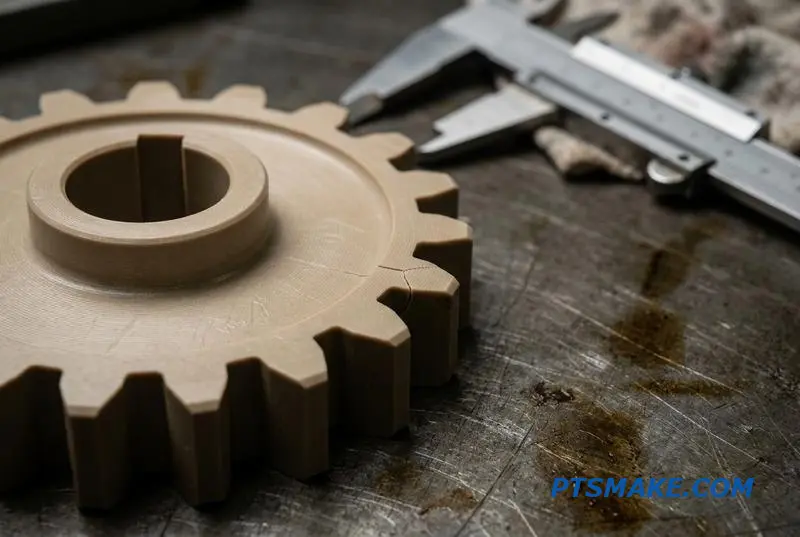
When performing PEEK CNC machining, material is removed, which disrupts the polymer’s internal structure and creates stress. Annealing is a controlled heating and cooling process that allows the material to relax, relieving this stress. This step is crucial for any part requiring tight tolerances or long-term stability.
Why Annealing Adds Cost and Time
The process requires specialized ovens and careful monitoring, which adds to both the cost and lead time. A typical peek stress relief annealing cycle can add a full day to production. Cheap suppliers often omit this, betting the part won’t fail immediately. This is a gamble you don’t want to take on critical components.
Deciding to Anneal
| Fattore | Justification for Skipping | Justification for Annealing |
|---|---|---|
| Tolleranza | Loose / Non-critical | Tight / ±0.05mm or less |
| Applicazione | Prototypes, fit-checks | Functional, load-bearing parts |
| Ambiente | Stable room temperature | Variable or high temperatures |
| Conseguenza del fallimento | Basso | High (e.g., medical, aerospace) |
The increased Cristallinità9 from annealing enhances mechanical properties. At PTSMAKE, we almost always recommend it for functional parts. You should always ask your supplier: "Is annealing included in this quote?"
Skipping the annealing process on machined PEEK is a false economy. It compromises dimensional stability and increases the risk of cracking. For reliable, high-performance parts, always confirm with your supplier that this critical stress-relief step is included in their process.
Machined PEEK vs Injection-Molded PEEK: Which Route Is Right?
Choosing between machining and injection molding for PEEK parts often comes down to volume. Many engineers default to molding, but for low-volume custom parts, this can be a costly mistake. PEEK CNC machining is the clear winner for prototypes and short production runs.
The Crossover Point
The key is understanding the cost and lead-time crossover. Machining avoids expensive tooling, making it faster and more affordable for initial quantities. Molding requires a significant upfront investment in molds, which only pays off at high volumes.
Initial Cost & Lead Time Comparison
| Processo | Costo degli utensili | Per-Part Cost (Low Volume) | Tempi di consegna (prototipi) |
|---|---|---|---|
| Lavorazione CNC | Nessuno | Più alto | Giorni |
| Stampaggio a iniezione | Alto | Più basso | Weeks to Months |
This trade-off is fundamental. For anything under a few hundred parts, the economics almost always favor PEEK CNC machining, especially when tight tolerances are a requirement.
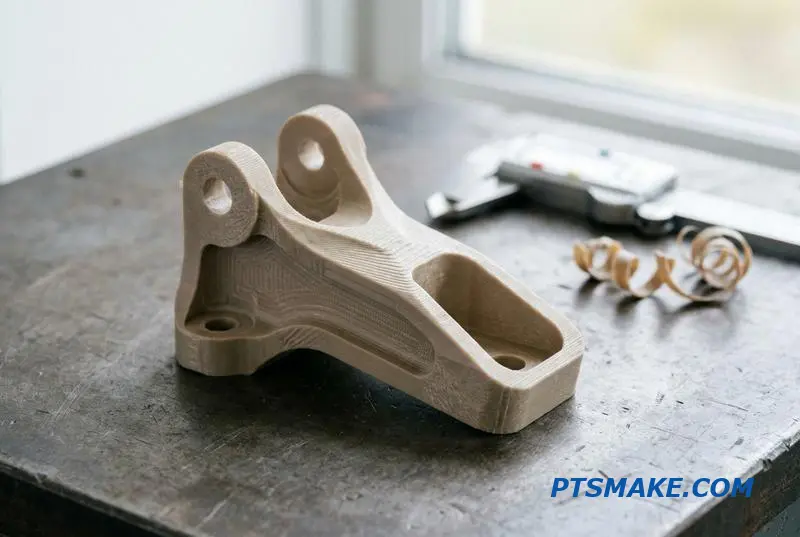
When to Machine PEEK
Beyond cost, performance is a critical factor. Machining from a solid stock material provides consistent mechanical properties and superior dimensional stability. This is essential for components where precision cannot be compromised. The process removes material, avoiding internal stresses common in molding.
Prototypes and Iterations
For rapid prototyping, machining is unbeatable. Design changes can be implemented immediately without waiting for new tooling. This agility is crucial in product development cycles where testing and refinement are constant. Each iteration is fast and cost-effective.
Complex Geometries & Tight Tolerances
Injection molding struggles with very sharp internal corners or undercuts without complex, expensive tooling. In our experience at PTSMAKE, peek cnc machining easily achieves tolerances as tight as ±0.005mm. Molded parts also exhibit some level of Anisotropia10 due to polymer flow during injection, which can affect performance.
Decision Matrix: Volume vs. Tolerance
| Part Volume | Loose Tolerance | Tolleranza stretta | Processo consigliato |
|---|---|---|---|
| 1-100 | Lavorazione meccanica | Lavorazione meccanica | Lavorazione CNC del PEEK |
| 100-1,000 | Machining/Molding | Lavorazione meccanica | Machining is often better |
| 1,000-10,000+ | Stampaggio | Molding/Machining | Molding is cost-effective |
This framework helps clarify why choosing the right process from the start saves both time and money.
For prototypes, low-volume runs, and high-precision parts, PEEK CNC machining provides speed, flexibility, and reliability. Injection molding only becomes the logical choice when production volume is high enough to justify the significant initial tooling investment and longer lead times.
PEEK Machining on a Mill vs a Lathe: Process Fit by Geometry
Choosing the right process for PEEK CNC machining depends entirely on the part’s geometry. A part’s shape dictates whether milling or turning is more efficient and cost-effective. Rotational symmetry is the key deciding factor.
Milling for Complex Geometries
Complex, non-symmetrical parts like manifolds or housings are best suited for PEEK milling. These components often have features on multiple faces that cannot be created on a lathe.
Turning for Symmetrical Geometries
Cylindrical parts, such as bushings, seals, and rings, are ideal for PEEK CNC turning. This process is highly efficient for producing parts with rotational symmetry, ensuring concentricity and a fine surface finish.
| Geometria della parte | Processo consigliato | Typical PEEK Parts |
|---|---|---|
| Prismatic, Asymmetrical | PEEK Milling | Housings, Valve Bodies, Manifolds |
| Rotational, Symmetrical | PEEK CNC Turning | Bushings, Seals, Rings, Insulators |
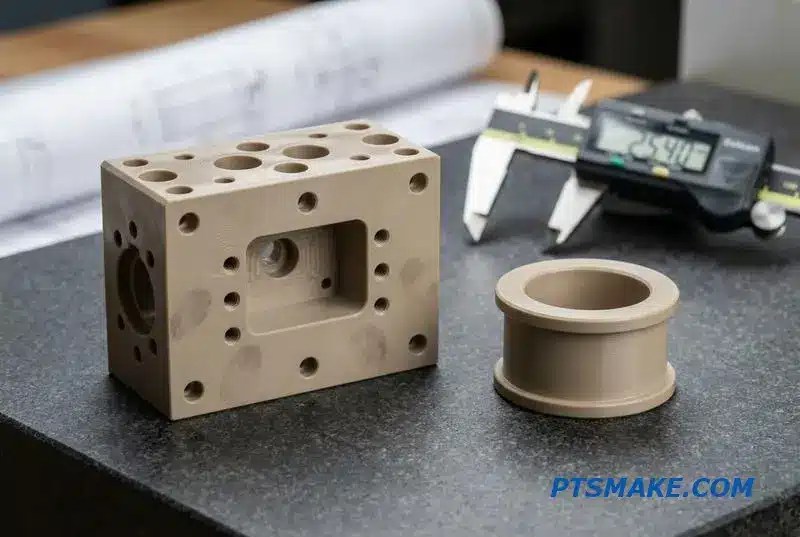
The choice becomes clearer when we look at the specific capabilities of each machine. For instance, 5-axis milling is essential for PEEK components with intricate features on multiple planes. It allows us to machine complex geometries in a single setup, minimizing handling and improving accuracy.
For PEEK turned parts, the efficiency of a CNC lathe is unmatched. It quickly produces components with uniform diameters and concentric features. The continuous cutting action also yields an excellent surface finish, which is often a critical requirement for seals and bearings.
Choosing the right partner involves asking specific questions about their capabilities. At PTSMAKE, we guide our clients through this process to ensure the most stable and cost-effective manufacturing method is chosen for their PEEK components. Effective Attrezzatura di lavorazione11 is also crucial, especially with PEEK’s tendency to deform under pressure.
Key Questions for Your Supplier
| Argomento | Domanda da porre | Perché è importante |
|---|---|---|
| Capacità della macchina | Do you have 5-axis milling or multi-axis turning capabilities for PEEK? | Confirms ability to produce complex geometries efficiently. |
| Utensili | What specific cutting tools do you use for PEEK? | The right tools prevent melting, burrs, and residual stress. |
| Esperienza | Can you share examples of similar PEEK parts you’ve machined? | Demonstrates relevant experience with the material and geometry. |
Choosing between milling and turning for PEEK parts is a geometry-driven decision. Selecting a supplier with the right equipment and experience is crucial. Asking targeted questions ensures your design intent is met with the most efficient and precise machining process available.
Prototype to Production: Scaling PEEK Parts Without Scrap Surprises
Scaling PEEK parts from a prototype to full production presents unique challenges. What works for a single part often fails at volume. The initial focus during peek prototype machining is simply proving the design’s form, fit, and function.
From One to One Thousand
The primary goal is validation. At this stage, standard tooling and conservative speeds and feeds are used. The cost per part is high, but the focus is on quick turnaround and design iteration, not manufacturing efficiency. This is a critical first step.
La sfida della scalabilità
When you need to scale cnc plastic parts, simply repeating the prototype process leads to high costs and inconsistent quality. Production demands efficiency, repeatability, and process control. This transition is where many projects encounter unexpected scrap and budget overruns if not planned carefully.
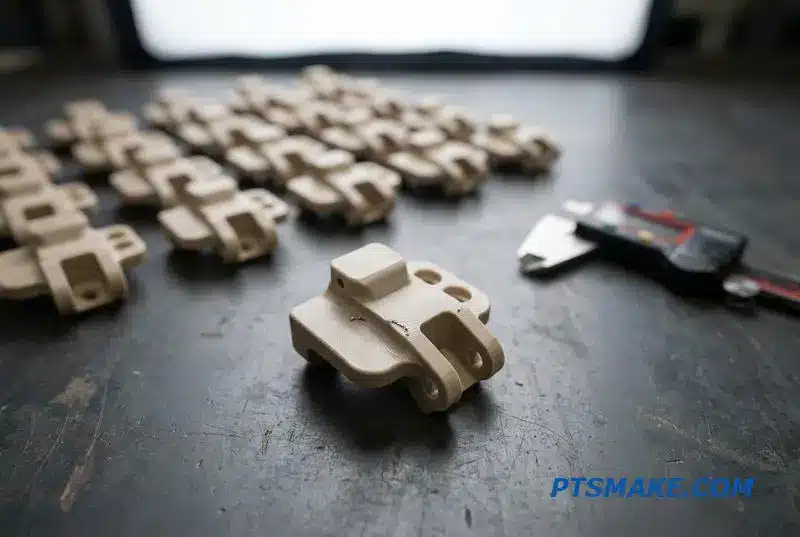
Moving into peek low volume production requires a shift in mindset and strategy. We move from proving a design to proving a process. This means optimizing every step for repeatability and efficiency. It’s not just about making more parts; it’s about making them identically and cost-effectively.
Process and Cost by Volume
The economics change dramatically with volume. For instance, creating custom workholding is not feasible for ten parts but becomes essential for one thousand. Likewise, machine setup time is a major cost driver for small batches but becomes negligible in high-volume runs. Post-machining processes like Ricottura12 are critical to control residual stress, ensuring stability in the final parts.
| Production Tier | Strategia di attrezzaggio | Focus sul processo | Costo per pezzo (relativo) |
|---|---|---|---|
| Prototipo (1-10) | Standard Vises & Jaws | Convalida del progetto | 100% |
| Basso Volume (50-500) | Soft Jaws, Simple Fixtures | Repeatability, Cycle Time | 40-60% |
| High-Volume (1000+) | Custom Fixtures, Automation | Massima efficienza | 15-30% |
At PTSMAKE, we help clients navigate this transition by planning for scale from day one. This proactive approach prevents costly surprises and ensures a smooth ramp-up. We focus on creating a robust manufacturing plan that evolves with your volume requirements.
Successfully scaling PEEK part production requires a strategic shift from design validation to process optimization. Planning for tooling, cycle time, and material stability from the start is essential to avoid surprises and control costs as volume increases.
When PEEK Is the Wrong Choice for Your Part
PEEK is a phenomenal material, but it’s not always the right answer. Over-engineering with PEEK can unnecessarily inflate project costs. The goal is to match the material to the application, not just to choose the most high-performance option available for your parts.
Understanding the Cost-Performance Trade-Off
Sometimes, a more common polymer is a better fit. For applications where extreme chemical or temperature resistance isn’t critical, other materials offer excellent performance at a fraction of the cost. Making the right choice is key for budget-conscious production runs.
PEEK vs. Acetal: A Quick Look
| Caratteristica | SETTIMANA | Acetale (POM) |
|---|---|---|
| Costo relativo | Alto | Basso |
| Lavorabilità | Buono | Eccellente |
| Temp. Max. | ~250°C | ~90°C |
This simple comparison shows why asking questions is so important.
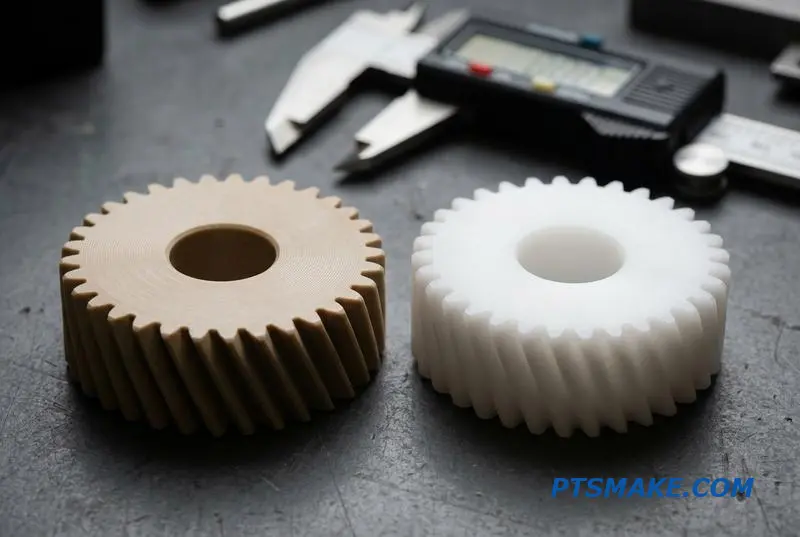
At PTSMAKE, we guide clients to the most effective material, ensuring they don’t pay for performance they don’t need. Honesty in material selection builds trust and leads to better long-term partnerships. Let’s explore when an alternative is the smarter choice.
Cost-Constrained Production Runs
For high-volume projects, material cost is a major factor. Acetal (POM) and Nylon offer great mechanical properties and are much more economical. They are often the best choice for gears, bushings, and structural components where PEEK’s elite traits are unnecessary.
When Temperature Isn’t a Challenge
PEEK shines in high-temperature environments. However, if your part operates below 90°C (194°F), Acetal is a strong candidate. PTFE is even better for extreme cold, but its mechanical strength is lower. Choosing a material with a suitable, not excessive, thermal range is smart engineering. Exceeding these limits can lead to Pirolisi13.
Specific Wear and Friction Needs
While PEEK has good wear resistance, it isn’t always the top performer. For low-friction applications like bearings or slide plates, PTFE is often superior. Its exceptionally low coefficient of friction makes it a specialized, and sometimes better, choice.
Material Trade-Off Matrix
| Materiale | Costo relativo | Max Temp. (°C) | Resistenza all'usura | Il migliore per |
|---|---|---|---|---|
| SETTIMANA | $$$$ | 250 | Molto buono | All-around high performance |
| Acetale (POM) | $ | 90 | Buono | General mechanical parts |
| PTFE | $$ | 260 | Good (Low Friction) | Low friction, chemical seals |
| Nylon 6/6 | $ | 95 | Eccellente | High-impact, wear pads |
This matrix helps clarify the best applications for each material in a peek cnc machining context.
Choosing the right material requires balancing performance needs and budget. While PEEK is a top-tier polymer, alternatives like Acetal, Nylon, or PTFE can offer a more practical and cost-effective solution for many CNC machining projects, delivering the required performance without over-engineering.
Understanding this property helps predict material behavior during machining and its performance in high-temperature applications. ↩
Understanding tribology helps engineers design more efficient and durable moving parts. ↩
Understanding this process helps select materials for high-temperature steam and water environments. ↩
Understanding this value helps engineers design for higher efficiency in moving mechanical systems. ↩
Discover how this property affects material choice for high-performance electrical insulators in critical applications. ↩
Understanding residual stress helps predict material failure in high-performance engineering applications. ↩
This value helps predict dimensional changes, crucial for high-precision applications in varying thermal environments. ↩
Understanding this property helps predict how materials form chips and burrs during CNC machining processes. ↩
Understanding this concept helps predict a polymer’s mechanical properties and thermal stability. ↩
Understanding this helps predict a material’s strength and behavior under stress from different directions. ↩
Understanding workholding methods helps evaluate a supplier’s ability to maintain precision on complex PEEK parts. ↩
Learn how this heat treatment reduces internal stress, preventing warping and improving dimensional stability in machined PEEK. ↩
Understanding this concept helps select materials that can withstand high-temperature applications without degrading. ↩