Skip conventional machining mistakes—when hardened steel meets sharp corners or thin walls, standard mills distort parts, burn cutters, and blow your budget on scrapped pieces.
EDM (Electrical Discharge Machining) uses controlled electrical sparks to erode conductive materials, cutting hardened steel, carbide, and complex geometries without mechanical force. It delivers sharp internal corners, tight tolerances down to ±0.005mm, and burr-free surfaces where conventional cutting fails.
I put this guide together because too many engineers pay for EDM they don’t need, or skip it when it’s the only real option. Below, I’ll walk you through when to choose EDM, what to spec on drawings, and how to get fair quotes.
When You Need EDM Instead of Conventional Machining
You know the moment. Your design features hardened steel that a standard end mill can’t touch. Or perhaps it has sharp internal corners, deep and thin slots, or a fragile geometry. These are clear signals pointing to when you need to use EDM machining.
Machining Extremely Hard Materials
Conventional tools struggle with materials above 45 HRC. EDM, however, machines any conductive material regardless of its hardness, including tool steels, tungsten carbide, and Inconel. This makes it ideal for molds, dies, and high-wear components.
Creating Complex Internal Geometries
If your part requires sharp internal corners with a radius smaller than what a cutting tool can achieve, EDM is the solution. It also excels at producing deep, narrow cavities and slots without the risk of tool breakage or deflection.
| Funktionell utmaning | Conventional Machining | EDM-lösning |
|---|---|---|
| Material Hårdhet | Limited to softer metals | Unaffected by hardness |
| Invändiga hörn | Limited by cutter radius | Can achieve sharp corners |
| Tunna väggar | Risk of distortion/damage | No-contact, stress-free |
| Burrs | Often requires deburring | Produces a burr-free finish |
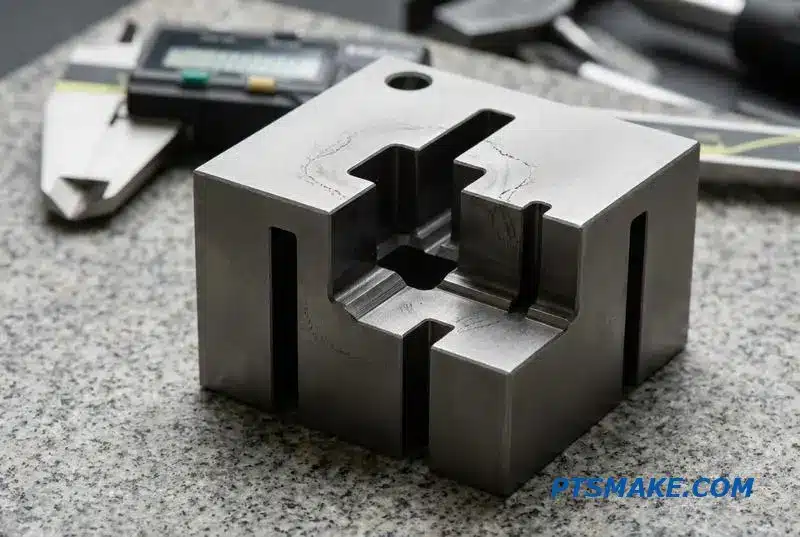
Conventional machining relies on physical force, where a cutting tool shears material away. This process generates heat, stress, and mechanical forces on the workpiece. For delicate parts or extremely hard materials, this force can cause distortion, micro-fractures, or tool failure, compromising the final part’s integrity.
The Non-Contact Advantage
EDM is a non-contact process. It uses electrical discharges to erode material, eliminating mechanical stress entirely. This is why it can machine fragile features like thin walls or honeycomb structures without causing them to deform or break. There is no tool pressure to worry about.
Precision Beyond Cutters
At PTSMAKE, we often use our EDM Machining Services for features that are simply impossible for a mill or lathe. Think of a deep pocket with a 0.1mm internal corner radius. No cutting tool can create that. The process relies on a precisely controlled spark in a Dielektrisk vätska1, which flushes away the vaporized material.
| Bearbetningsmetod | Force Application | Suitable Geometries |
|---|---|---|
| CNC-fräsning/-svarvning | Direct Mechanical Contact | External surfaces, rounded corners |
| EDM (Electrical Discharge) | No-Contact (Spark Erosion) | Hard materials, sharp internal corners |
This fundamental difference is why EDM isn’t just an alternative; it’s an enabling technology for advanced component design that pushes the boundaries of manufacturing.
When conventional machining methods face limitations due to material hardness, intricate internal geometries, or delicate structures, EDM provides a precise, non-contact solution. It excels where traditional tools would fail, enabling complex designs with tight tolerances and burr-free finishes.
Wire EDM vs Sinker EDM vs Hole Drilling — Which Process Fits Your Part
Choosing the right Electrical Discharge Machining (EDM) process is critical for achieving the required precision and cost-effectiveness. Each method—Wire, Sinker, and Hole Drilling—excels in specific applications. Understanding their unique capabilities ensures your part meets specifications without unnecessary expense or production delays.
Förstå de grundläggande skillnaderna
At PTSMAKE, we guide clients through this decision daily. Wire EDM is ideal for cutting precise 2D profiles through conductive materials. Sinker EDM creates complex 3D cavities, while Hole Drilling EDM specializes in small, deep holes that are difficult or impossible to produce with traditional drills.
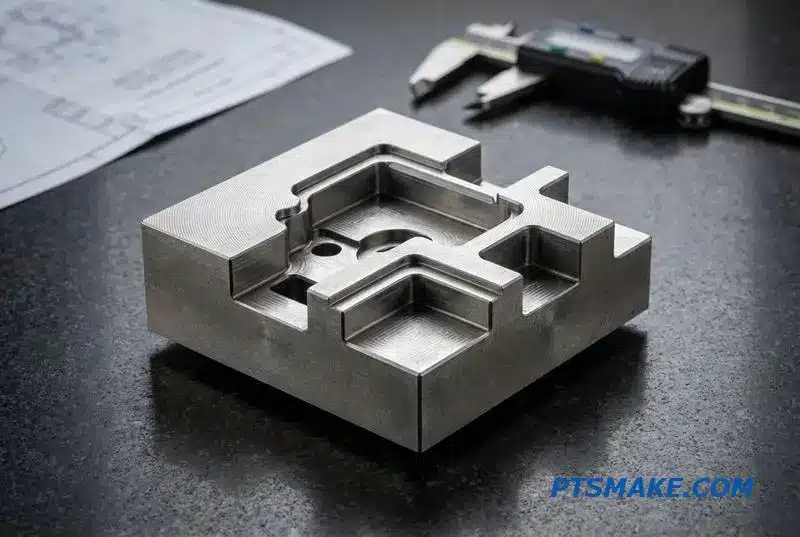
When evaluating wire vs sinker EDM, the primary factor is part geometry. Wire EDM acts like a bandsaw, using a thin wire to cut through the entire thickness of a workpiece. It is perfect for creating punches, dies, and intricate outlines with sharp internal corners.
Sinker and Hole Drilling Applications
Sinker EDM, or Ram EDM, uses a custom-shaped electrode to "sink" into the material, eroding a cavity that mirrors the electrode’s shape. This makes it essential for mold making, creating blind pockets, and features with complex 3D surfaces that don’t pass through the part. A key challenge is managing electrode wear.
Hole Drilling EDM is a specialized, high-speed process. We use it to create starter holes for Wire EDM or to drill fine cooling channels in hardened tool steels. The process is fast and precise, even with high aspect ratios. A byproduct of all EDM processes is the Recast layer2, which needs consideration for fatigue-critical applications.
Process Selection Guide
Based on our tests with various client projects, this table helps map features to the best EDM Machining Services.
| Funktionstyp | Recommended EDM Process | Typisk tolerans | Typisk ytfinish (Ra) |
|---|---|---|---|
| Through-Cutting, 2D Profiles | Trådgnistning | ±0,005 mm | 0.4 µm |
| 3D Cavities, Blind Pockets | Sinker EDM | ±0,010 mm | 0,8 µm |
| Small, Deep Holes | Hole Drilling EDM | ±0,025 mm | 1.6 µm |
| Extrusion Dies | Trådgnistning | ±0,005 mm | 0.4 µm |
The choice between Wire, Sinker, and Hole Drilling EDM depends entirely on your part’s geometry. Wire EDM is for 2D through-cuts, Sinker EDM is for 3D cavities, and Hole Drilling is for small, deep holes. Matching the process to the feature is key.
EDM Tolerances and Surface Finish — What to Expect and Spec
Electrical Discharge Machining (EDM) offers incredible precision, but it’s crucial to understand its limits to spec parts effectively. Over-specifying tolerances or finishes on non-critical features is a common mistake that drives up costs without adding value. Let’s look at what is realistically achievable.
Wire EDM Capabilities
Wire EDM is known for its high accuracy. With a single rough pass, you can expect a tolerance of around ±0.025 mm. However, by adding multiple trim passes, we can significantly refine both the dimensional accuracy and the surface finish, making it a reliable process for intricate parts.
Sinker EDM Capabilities
Sinker EDM accuracy depends heavily on the quality of the electrode and flushing efficiency. The process creates a cavity by eroding material, so any imperfection in the electrode will be mirrored in the workpiece. Proper flushing is vital to remove debris and ensure a consistent spark gap.
| Maskineringstyp | Typisk tolerans (mm) | Typical Surface Finish (Ra, µm) |
|---|---|---|
| Wire EDM (1 Pass) | ±0.025 | 1.6 – 2.5 |
| Wire EDM (3-5 Passes) | ±0.005 | 0.2 – 0.4 |
| Sinker EDM (Fine) | ±0.010 | 0.4 - 0.8 |
Understanding the trade-offs between precision and cost is key. Every additional trim pass in Wire EDM increases machine time, which directly translates to higher costs. While we can achieve a mirror-like finish, it is not always necessary for the part’s function.
The Cost of a Finer Finish
The relationship between surface finish and cost is not linear. Improving the finish from 0.8 Ra to 0.4 Ra might require two or three extra passes. This additional machine time is the primary cost driver in our EDM Machining Services.
| Number of Passes | Ytfinish (Ra, µm) | Relativ kostnad |
|---|---|---|
| 1 (Rough) | ~2.5 | 1x |
| 2 (Rough + Skim) | ~1.2 | 1.5x |
| 4 (Rough + 3 Skims) | ~0.4 | 3x |
Specifying for Sinker EDM
For Sinker EDM, the process is equally sensitive. The precision of the final part is directly linked to the quality of the graphite or copper electrode. Imperfections and Electrode wear3 during the process can affect the final dimensions. Effective flushing is also critical to prevent debris from causing secondary discharges that mar the surface.
How to Specify on Your Drawings
When preparing a drawing, clearly mark the critical surfaces that require a high-quality EDM machining tolerance surface finish. For non-critical internal features or clearance holes, a standard finish is usually sufficient. This approach ensures you only pay for the precision you truly need. At PTSMAKE, we often work with clients to optimize these specifications.
Achieving tight tolerances and fine surface finishes with EDM is entirely possible but comes at a cost. Specify precision only where it is functionally required to manage your budget effectively. Smart specification is key to leveraging EDM’s full potential without overspending.
Materials EDM Can Cut — and the Surprising Limits
The fundamental rule for Electrical Discharge Machining (EDM) is simple: the material must conduct electricity. This process isn’t about physical force; it uses thermal energy from electrical sparks to erode the workpiece. This makes it ideal for materials that are too hard for traditional machining.
What Works Best with EDM
Any conductive metal is a candidate for our EDM Machining Services. Hardened tool steels, titanium, and superalloys are where this technology truly excels. These materials often pose significant challenges for conventional milling or turning, but EDM handles them with precision.
Common Conductive Materials
| Materialgrupp | Exempel | EDM Suitability |
|---|---|---|
| Stål | Tool Steel, HSS, Stainless | Utmärkt |
| Superlegeringar | Inconel, Hastelloy | Utmärkt |
| Icke-järnhaltiga | Copper, Aluminum, Brass | Bra |
| Hard Metals | Tungsten Carbide, Titanium | Utmärkt |
The Surprising Limits
Conversely, EDM cannot machine non-conductive materials. This is a common point of confusion. Materials like ceramics, glass, most plastics, and composites are invisible to the EDM process because they cannot complete the electrical circuit required for sparking.
The effectiveness of EDM is directly tied to a material’s conductivity. A lack of this property makes the process impossible. This is why we can’t use it on materials like glass or ceramics, which act as insulators and prevent the necessary spark erosion from occurring. This is a key factor when planning a project.
Hard vs. Soft Materials
EDM truly shines when machining extremely hard materials. After heat treatment, metals like hardened tool steel or tungsten carbide become very difficult to mill conventionally. EDM, however, is unaffected by hardness, making it the perfect solution for creating complex features in these tough materials.
On the other hand, softer materials like aluminum can be machined much faster using traditional CNC milling. However, we still rely on EDM for aluminum parts when a design calls for sharp internal corners or deep, narrow cavities that a standard cutting tool cannot produce.
Jämförelse av applikationer
| Materialtyp | Conventional Machining | EDM Application |
|---|---|---|
| Härdat stål | Difficult, slow, high tool wear | Ideal for complex shapes, fine details |
| Aluminium | Fast, efficient | Niche use for sharp corners, deep slots |
| Tungsten Carbide | Nearly impossible | Primary method for shaping |
Begreppet Electrical resistivity4 is critical here. Materials with low resistivity (high conductivity) are excellent for EDM, while those with high resistivity are not viable. This simple property dictates the entire scope of what our EDM machining services can accomplish.
Conductivity is the absolute requirement for EDM. The process excels on hard metals that are challenging to mill but also serves specific purposes for softer materials, such as creating sharp internal corners where conventional tools cannot reach.
What EDM Costs Per Part — and What Drives the Price
Understanding the cost of Electrical Discharge Machining (EDM) is not always straightforward. The price is not just based on machine time. Key factors like setup complexity, material type, and the required surface finish significantly impact the final cost per part.
Viktiga kostnadsfaktorer
Many elements contribute to the final quote. These include the time to program the machine, the number of operations, and the consumption of materials like wire or graphite for electrodes. My goal here is to clarify these drivers for you.
Why It’s Worth It
While often having a higher hourly rate than CNC milling, EDM creates features that are otherwise impossible. It enables sharp internal corners, deep ribs, and complex geometries in hardened materials, providing unique value.
Djupare dykning i kostnadsdrivare
The EDM machining cost per hour is a useful metric, but it only tells part of the story. The initial setup, for instance, can be a significant one-time cost, especially for complex parts requiring custom fixtures. This is a common point of discussion with clients at PTSMAKE.
Sinker vs. Wire EDM Costs
Sinker EDM requires a custom electrode, which must be precisely machined first. This "pre-machining" step adds considerable cost and time. Wire EDM consumes brass wire as it cuts, and the cost depends on the total path length and wire diameter used for the job.
The Role of Precision
The number of trim passes directly affects both precision and cost. A single rough pass is quick, but achieving a fine surface finish and tight tolerances requires multiple, slower trim passes. This increases machine time but ensures quality. The underlying process relies on Faradays lagar om elektrolys5 for material removal.
| Kostnadsdrivare | Påverkan på priset | Anteckningar |
|---|---|---|
| Inställningstid | Medelhög-Hög | Higher for complex geometries or first-time runs. |
| Electrode Machining | High (Sinker EDM) | The electrode is a custom-machined tool itself. |
| Maskintid | Hög | Typically the largest component of the total cost. |
| Trim Passes | Medium | More passes equal higher precision and higher cost. |
This breakdown helps clarify why two seemingly similar parts can have very different costs when using EDM Machining Services.
EDM costs are driven by setup, machine time, materials, and precision requirements. Understanding these elements allows for better budgeting and fair quote comparison, ensuring you pay for the unique capability to create features impossible with other methods.
Surface Finish Levels and Recast Layer — What Engineers Must Know
Electrical Discharge Machining (EDM) is highly precise. However, it creates a unique surface condition. Engineers must understand the recast layer, a thin, brittle surface that forms as molten material resolidifies. This layer can be a major concern for performance.
The Challenge of the Recast Layer
This "white layer" is extremely hard but can contain micro-cracks. For parts under cyclical stress, these cracks can lead to premature failure. Ignoring this detail can compromise the integrity of critical components, a risk we always address in our EDM Machining Services.
Managing Surface Integrity
Below is a quick overview of how the recast layer thickness is affected by different EDM passes.
| EDM Pass Type | Typical Recast Layer Thickness | Ytfinish (Ra) |
|---|---|---|
| Grovbearbetning | 15-50 µm | 3.2-6.3 µm |
| Semi-Finishing Pass | 5-15 µm | 0,8-1,6 µm |
| Finbearbetning | 1-5 µm | 0,2-0,8 µm |
Managing the recast layer is about choosing the right post-processing strategy. At PTSMAKE, we guide clients on the best approach for their application. The goal is to control the EDM recast layer surface finish without adding unnecessary cost or complexity to your project.
Options for Recast Layer Removal
Multiple trim or skim passes are the first line of defense. Each subsequent pass uses lower energy, removing the recast layer from the previous pass and creating a much thinner one. For applications requiring complete removal, secondary operations are necessary.
Sekundära operationer
Polishing or grinding can mechanically remove the layer. For some materials, a subsequent light machining pass or even specific heat treatments can effectively eliminate the layer and relieve surface stress. We often discuss these trade-offs with our clients to find the right balance.
When is the Recast Layer a Problem?
For fatigue-critical parts in aerospace or medical devices, the recast layer is unacceptable. Its micro-cracks are failure initiation points. The material properties below this layer, in the värmepåverkad zon6, are also altered. You must specify its removal on the drawing.
| Tillämpningstyp | Recast Layer Tolerance | Rekommenderad åtgärd |
|---|---|---|
| Komponenter för flyg- och rymdindustrin | Not acceptable | Multiple trim passes + polishing |
| Medicinska implantat | Not acceptable | Full removal via secondary machining |
| General Tooling | Often acceptable | Minimal trim passes |
| Injection Molds | Varies by finish req. | Finishing passes sufficient |
For non-critical components where surface hardness is a benefit and fatigue is not a concern, the recast layer can sometimes be left in place.
Understanding the EDM recast layer is crucial for component reliability. Strategic trim passes can reduce it, while secondary operations remove it entirely. Specifying your requirements clearly ensures parts meet performance demands, especially in critical applications.
Sharp Corners, Deep Slots, and Thin Walls — What EDM Does Best
Traditional CNC milling has physical limits. A rotating cutter will always leave a radius in an internal corner, forcing design compromises. This is where EDM machining services excel, creating features impossible with other methods.
The Problem with Physical Tools
Milling cutters cannot machine what they cannot reach. The smallest internal radius is dictated by the tool’s diameter. This simple fact can limit a part’s functionality, especially in mold and die making where sharp corners are often essential for the final product shape.
Unlocking Design Freedom
EDM works without physical cutting force, using electrical discharges to erode metal. This non-contact process opens doors to complex geometries. It’s a fundamental shift in how we approach the manufacturing of intricate parts.
| Geometrisk utmaning | Milling Limitation | EDM-lösning |
|---|---|---|
| Invändiga hörn | Cutter radius dictates corner shape | True, sharp corners with near-zero radii |
| Deep Slots | Tool breakage and deflection risk | High aspect ratio slots are possible |
| Tunna väggar | Wall deflects or breaks under force | No cutting forces, preserving fragile features |
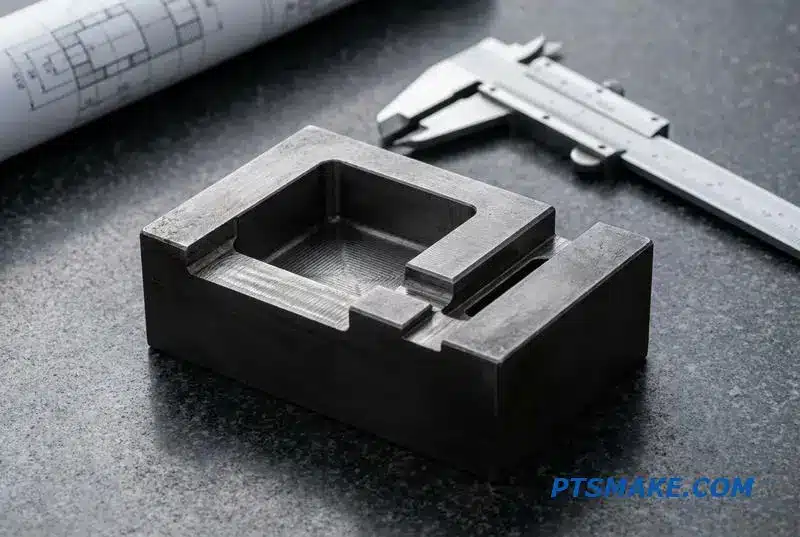
For an engineer, Electrical Discharge Machining is more than just a process; it’s a gateway to better designs. It removes the constraints imposed by cutting tools, allowing you to design for function first. This is especially true when working with tough, hardened materials.
Post-Heat-Treat Machining
One of the most powerful applications is machining components after they’ve been heat-treated. You can create precise square pockets in a fully hardened D2 tool steel die without introducing stress or affecting the material’s temper, something that is simply not feasible with milling.
High-Ratio Geometries
Think about creating deep, narrow slots for cooling channels inside an injection mold. A traditional endmill would snap. With EDM, we can create features with a very high Aspect-förhållande7, which is critical for efficient thermal regulation and producing high-quality molded parts.
Komponenter för tunna väggar
I’ve seen projects involving parts with delicate webs or fins that would instantly deform under milling pressure. EDM’s non-contact nature makes it ideal for producing these thin, fragile walls with precision. This is essential for components in aerospace and medical devices.
EDM is the definitive solution for geometries that conventional machining cannot handle. It enables the creation of sharp corners, deep slots, and thin walls in hardened materials, turning complex design challenges into tangible, high-performance components for our clients at PTSMAKE.
Burr-Free and Stress-Free: The Hidden Benefits of EDM
When people consider our EDM Machining Services, they often focus on precision. However, two of the most significant advantages are often overlooked: the process is completely burr-free and stress-free. This is because EDM uses thermal energy, not mechanical force, to remove material.
The Problem with Mechanical Force
Conventional machining physically cuts material, which can introduce stress, create burrs, and cause deflection in thin or delicate parts. These issues lead to secondary operations like deburring and can even cause part failure down the line, increasing costs and lead times.
EDM’s Non-Contact Advantage
Our EDM burr-free stress-free machining avoids these problems entirely. The non-contact nature preserves the integrity of even the most fragile workpieces.
| Funktion | Conventional Machining | EDM-bearbetning |
|---|---|---|
| Kontakt | Direct physical contact | No physical contact |
| Burrs | Common, requires deburring | Ingen |
| Stress | Induces mechanical stress | Minimal thermal stress |
| Känsliga delar | High risk of distortion | Safe and precise |
This makes EDM an ideal solution for components where quality and reliability cannot be compromised.
Beyond the obvious precision, the true value of EDM lies in its gentle touch. I’ve seen projects where conventional methods were not feasible due to the risk of part distortion or the high cost of manual deburring on complex internal features. EDM was the only viable path forward.
Eliminering av sekundära operationer
A major cost-saving benefit is the elimination of the deburring step. For intricate parts with many small features, deburring can be a time-consuming and expensive manual process. With EDM, the parts come off the machine ready for the next stage, which simplifies the entire production workflow.
Preserving Material Integrity
The absence of mechanical force is critical for maintaining the workpiece’s structural integrity. We have found that conventional cutting can alter the Material Temper8 near the cut surface, potentially weakening the component. EDM’s process avoids this, ensuring the material properties remain consistent throughout the part. This is particularly important for aerospace and medical applications where material performance is paramount.
| Förmån | Påverkan på produktionen |
|---|---|
| No Deburring | Reduced labor costs and faster cycle times |
| No Stress | Improved part reliability and performance |
| No Distortion | Lower scrap rates for fragile components |
| Processtyrning | Higher consistency and repeatability |
By choosing EDM, you are not just getting a precise cut; you are investing in a higher-quality, more reliable final product with a lower total cost of manufacturing.
EDM Machining Services offer more than just precision. By eliminating burrs and mechanical stress, the process reduces secondary operations and scrap rates. This translates directly into higher quality parts and significant cost savings, especially for complex and delicate components.
When EDM Is the Wrong Choice — Save Money by Not Using It
Electrical Discharge Machining (EDM) is a powerful tool for complex geometries and hard materials. However, it’s not a one-size-fits-all solution. Knowing when to avoid it is just as important as knowing when to use it. The key is understanding its primary limitation: speed.
Slow Material Removal Rate
The material removal rate in EDM is significantly slower than conventional milling or turning. For large, simple features or bulk material removal, this translates directly into longer cycle times and higher costs. Choosing the wrong process can inflate your budget unnecessarily.
When Conventional Machining Wins
For certain applications, traditional CNC machining is faster, more efficient, and more cost-effective. It’s crucial to evaluate your project’s specific needs before defaulting to a more advanced process.
| Scenario | Bästa processen | Anledning |
|---|---|---|
| Large, simple pockets | Konventionell fräsning | Faster material removal |
| Soft materials (e.g., Aluminum) | Konventionell fräsning | High-speed cutting capability |
| High-volume simple parts | CNC Turning/Milling | Lower cycle time per part |
Deciding on the right manufacturing process requires a careful balance of complexity, material, volume, and cost. While our EDM Machining Services at PTSMAKE excel at creating intricate features with tight tolerances, I always advise clients to consider alternatives for simpler jobs. The goal is efficiency.
Analyzing Cost vs. Complexity
The core principle is simple: use EDM for complexity that conventional tools cannot achieve. For straightforward parts, especially in high volumes, the setup and slow cutting speed of EDM make it economically impractical. We help our partners analyze this trade-off to ensure the best value.
When Not to Use EDM
High-Volume Simple Parts: For mass production of components without complex features, conventional CNC machining offers a much lower cost per part and faster turnaround. The economics do not favor EDM in this scenario.
Large-Scale Material Removal: If your primary goal is to quickly remove a large volume of material, EDM is the wrong choice. Conventional roughing passes with a milling machine are far more efficient, though they can introduce Härdning av arbetet9.
Non-Conductive Materials: This is a fundamental limitation. EDM works by creating an electrical discharge between the electrode and the workpiece. Therefore, it cannot be used on non-conductive materials like plastics, ceramics, or composites.
| Faktor | Favoring Conventional Machining | Favoring EDM |
|---|---|---|
| Geometri | Simple shapes, large features | Complex internal cavities, sharp corners |
| Material | Soft metals, non-conductive | Hardened tool steels, exotic alloys |
| Volym | Produktion av stora volymer | Prototypes, low-volume complex parts |
Choosing the right process is critical for budget and timeline. While EDM is an advanced solution, conventional machining is often faster and more cost-effective for straightforward jobs. Understanding when not to use EDM is key to optimizing your manufacturing strategy.
EDM Combined with CNC Machining — Getting the Best of Both
For parts with complex geometries, a single manufacturing process often falls short. The smartest approach is a hybrid one, using the strengths of different methods. This is where combining traditional CNC milling with precision EDM Machining Services provides a superior solution for challenging components.
The Best of Both Worlds
CNC milling is fast and efficient for removing large amounts of material. It quickly shapes the main body of a part. EDM, on the other hand, excels at creating features that are difficult or impossible for milling cutters to produce, especially in hardened materials.
Process Breakdown
| Process | Primär funktion | Idealisk för |
|---|---|---|
| CNC-fräsning | Avlägsnande av bulkmaterial | General shaping, pockets, holes |
| Trådgnistning | Fine detail cutting | Sharp internal corners, deep slots |
This combination allows us to machine parts efficiently without compromising on the intricate details or material properties, optimizing both speed and precision.
Why a Single Partner is Crucial
The real value of this hybrid method is unlocked when managed by a single, full-service supplier. When you use one partner for both processes, you get one drawing, one inspection report, and one point of responsibility. This eliminates the risk of miscommunication between different shops.
A Practical Example: Hardened Tooling
Consider a hardened tool steel injection mold. First, we use CNC milling to machine the main cavity and core structures while the material is still soft. After heat treatment, the steel is too hard for conventional cutters. We then use wire EDM to cut the sharp corners, ejector pin holes, and fine cooling channels with extreme precision.
Single-Source vs. Multi-Source Workflow
| Aspekt | Single Partner (PTSMAKE) | Flera leverantörer |
|---|---|---|
| Responsibility | Fully accountable | Potential for blame-shifting |
| Kommunikation | Streamlined & clear | Risk of data loss/errors |
| Kvalitetskontroll | Consistent inspection | Varied standards & reports |
| Ytans integritet10 | Controlled throughout | Disjointed process control |
Managing the EDM and CNC machining combined workflow under one roof at PTSMAKE ensures seamless transitions and total quality control. We handle the entire process, so you don’t have to.
Combining CNC for bulk removal and EDM for fine details is the most effective strategy for complex, hardened parts. A single partner streamlines this process, ensuring quality and accountability while simplifying your supply chain management from start to finish.
Design for EDM — Drawings That Machine Cleanly and Cost Less
Effective Electrical Discharge Machining (EDM) starts on the drawing board. Simple design choices can dramatically cut machining time and costs. By optimizing features for the EDM process, you get cleaner parts faster and more affordably. Small adjustments make a big difference.
Key Principles for Cost-Effective Design
An actionable EDM design for manufacturability guide focuses on practicality. Always provide corner radii where possible, as sharp internal corners require more complex electrode work or slower wire speeds. Looser tolerances on non-critical surfaces also reduce setup and machining time significantly.
Feature Comparison for EDM
This table shows how small design changes impact manufacturing.
| Designval | Good Practice (Lower Cost) | Poor Practice (Higher Cost) |
|---|---|---|
| Invändiga hörn | Generous radius (e.g., > 0.5mm) | Sharp, 90-degree corner |
| Toleranser | ±0.05mm on non-mating faces | ±0.005mm on all surfaces |
| Start Point | Pre-drilled start hole provided | No entry point for wire |
Designing for our EDM Machining Services requires thinking about the entire process. A well-designed part simplifies setup and execution, directly translating into savings. For instance, always design an entry point or start hole for wire EDM operations. This eliminates a secondary drilling process.
Optimizing Surface Finish and Tolerances
Specify trim passes only where the surface finish is critical for function. Each additional pass adds significant time. Unnecessarily tight tolerances on non-functional surfaces force us to slow down the process, increasing electrode wear and monitoring time, which adds to the final cost. Based on our client collaborations, smart tolerancing can reduce part cost by up to 30%.
Förstå bildförhållanden
Keep the aspect ratio of holes and slots practical. A very deep, narrow slot is difficult to flush, leading to slower cutting speeds and potential inaccuracies. This is because debris can’t escape efficiently, causing instability in the spark. This can also introduce surface defects like Microcracking11, which compromises part integrity.
Design Contrast: Cost Impact
A part designed with generous radii, practical tolerances, and a start hole can be machined much faster than one with sharp corners and unnecessarily tight specs everywhere. The difference isn’t minor; a well-designed part can often be produced for 20-40% less.
Smart EDM design for manufacturability focuses on practical choices like corner radii, tolerances, and entry points. These considerations directly reduce machining complexity and cost, ensuring you receive high-quality parts efficiently. At PTSMAKE, we guide our partners through these simple yet impactful optimizations.
Fixturing and Setup in EDM — How It Affects Your Lead Time
Many assume Electrical Discharge Machining (EDM) setup is similar to CNC milling. However, the fixturing and preparation are fundamentally different, directly impacting your project’s lead time. Unlike milling, EDM is a non-contact process that requires unique workholding solutions to ensure electrical conductivity and stability.
Key Setup Distinctions
The primary differences stem from the process itself. Wire EDM needs a clear path for the wire, and sinker EDM requires a custom electrode. Each step adds time before cutting even begins. These preparatory stages are crucial for the precision our EDM Machining Services deliver.
Initial Time Investment
| Setup Factor | CNC-fräsning | Electrical Discharge Machining (EDM) |
|---|---|---|
| Hållare för arbetsstycken | Mechanical clamping (vises, chucks) | Conductive, non-obstructive fixtures |
| Verktyg | Standard end mills, drills | Custom-machined electrodes (Sinker) |
| Pre-Processing | Minimal, locate part zero | Drill starter holes (Wire), machine electrode |
This initial investment in setup is a significant factor in the overall EDM setup fixturing lead time.
Understanding the nuances of EDM setup is key to managing project timelines effectively. Unlike simply clamping a block in a vise for milling, each EDM method has unique preparatory needs that add steps to the manufacturing process. These steps are non-negotiable for achieving high precision.
Wire EDM Setup Nuances
For wire EDM, we must first machine a "starter hole." The wire must be threaded through this hole to begin cutting. Additionally, fixtures cannot obstruct the wire’s path, which often requires creative workholding that avoids contact with the top or bottom surfaces of the workpiece.
Sinker EDM’s Extra Step
Sinker EDM requires a precisely machined electrode, which is essentially a mirror image of the final feature. This electrode must be manufactured first, usually through CNC milling. This adds an entire manufacturing process before the EDM work can even start, extending the lead time.
The Challenge of Multiple Setups
If a part requires features on multiple faces, each re-fixturing introduces new setup time. Every repositioning demands meticulous realignment to maintain accuracy. This process is sensitive to factors like Termisk expansion12, which can affect part dimensions during long machining cycles. To streamline this, consider consolidating features onto a single plane or providing starter holes in your design files. This simple foresight can significantly reduce production time.
Proper EDM fixturing and setup, though time-consuming, are foundational to precision. Understanding these steps—from creating starter holes to machining electrodes—helps clarify why lead times differ from conventional milling and how design choices can expedite your project.
Prototyping with EDM — From One-Off to Production Runs
Electrical Discharge Machining (EDM) is an excellent choice for prototypes, especially with complex geometries or hardened metals. Conventional tools often struggle with these jobs. EDM provides a precise solution without stressing the material. This makes it ideal for creating that first perfect part.
Why Start with EDM?
EDM cuts intricate shapes that are impossible for milling or turning. It works on materials after they have been heat-treated. This preserves the part’s final properties from the very beginning, ensuring the prototype accurately reflects the production unit.
Key Advantages for Prototypes
We have found that using EDM Machining Services for initial parts offers distinct benefits. It allows designers to test concepts with production-grade materials and hardness levels immediately. This avoids surprises later in the development cycle.
| Funktion | EDM Prototyping | Traditional CNC |
|---|---|---|
| Material Hårdhet | No limitations | Limited by tool material |
| Komplex geometri | Excellent for sharp corners | Difficult or impossible |
| Verktygsslitage | Minimal electrode wear | Significant tool wear |
| Inställningstid | Måttlig | Snabb för enkla delar |
Moving from a single prototype to a production run with EDM is a smooth process. The fundamental parameters established for the first part remain consistent for subsequent units. This ensures that the tenth or hundredth part is identical to the first, a key requirement for quality control.
Scaling Up: The EDM Path
The real benefit of EDM prototyping low volume production is scalability. The same setup used to create one piece can produce a small batch without major changes. This is perfect for initial market testing or for products with lower demand, where investing in expensive tooling for other processes is not justified.
Knowing When to Switch
EDM is not the fastest process. Its materialavverkningshastighet13 is lower than conventional CNC machining. When production volumes reach thousands of units, its cycle time can increase costs. At that point, processes like stamping or die-casting might be more economical.
| Produktionsvolym | Rekommenderad process | Viktiga överväganden |
|---|---|---|
| 1 - 100 | EDM | High precision, consistent quality |
| 100 – 1,000 | EDM or CNC Milling | Balance of cost and complexity |
| 1,000+ | Stamping, Casting | Höga initiala verktygskostnader |
Choosing a partner who understands this entire path is vital. At PTSMAKE, we guide clients from prototype to production. This ensures the design integrity is maintained, avoiding the costly and time-consuming process of re-qualification with a new supplier.
EDM is a highly effective method for transitioning from a single prototype to low-volume production. It ensures consistency and precision. Working with a single supplier who can manage this entire workflow streamlines the process and avoids costly re-qualification issues.
Quality Inspection of EDM Parts — What Reports to Demand
Ensuring the quality of EDM parts goes beyond a simple visual check. You need concrete data to verify that specifications are met. The right documentation confirms precision and consistency, which is fundamental for high-performance components.
The Essential QC Reports
For any EDM project, I always expect to see a standard set of reports. These documents provide objective evidence of quality and are non-negotiable for critical parts. They form the basis of a solid quality assurance process.
| Report Type | Syfte |
|---|---|
| CMM Report | Verifies critical dimensions and geometric tolerances. |
| Ytfinish (Ra) | Confirms the required texture and smoothness. |
| Recast Layer Check | Validates material integrity post-machining if specified. |
First-Article Inspection is Key
EDM is a highly repeatable process. Once the machine program and setup are validated, subsequent parts are very consistent. This makes the First-Article Inspection (FAI) the most critical step. A thorough FAI report ensures the entire batch will be correct.
A proper EDM quality control inspection framework relies on asking the right questions and demanding the right proof. It’s not about distrust; it’s about building a partnership based on verifiable data and clear communication.
Drilling Down on Documentation
A Coordinate Measuring Machine (CMM) report is essential for parts with complex geometries or tight tolerances. It provides a detailed 3D map of the part, confirming features that cannot be measured with calipers. For surface finish, ask how the supplier measures it; a profilometer provides a quantifiable Ra value, not just a visual comparison.
When applications require it, confirming the absence or controlled thickness of a recast layer is vital. This often requires specialized analysis. The entire process is a practical application of Metrologi14, ensuring every measurement is accurate and traceable. At PTSMAKE, we provide these reports as standard practice for our EDM machining services.
Key Questions for Your Supplier
Use these questions to gauge a potential supplier’s quality process. Their answers will reveal a lot about their commitment to quality.
| Fråga | Vad den avslöjar |
|---|---|
| Do you provide CMM reports? | Their capability to verify complex dimensional accuracy. |
| How do you verify surface finish? | Their equipment and process for meeting texture specs. |
| What is your typical scrap/rework rate? | Their overall process control and efficiency. |
A low scrap rate often indicates a mature and stable manufacturing process, which is exactly what you want from a partner providing reliable EDM machining services.
For effective EDM quality control, insist on key reports like CMM, surface finish, and recast layer verification. A thorough First-Article Inspection is crucial, followed by batch sampling, ensuring consistent quality for the entire production run.
EDM for Tooling vs Production Parts — Two Different Conversations
When discussing EDM Machining Services, the first question I ask is whether the project is for tooling or a production part. The answer completely changes the conversation, from the supplier you need to the metrics for success. These are two fundamentally different use cases.
Tooling: Built for Longevity
For tooling like molds, dies, and punches, EDM is often the primary method for hardened tool steels. Here, the focus is on precision, surface finish, and durability. A tool must last for thousands or even millions of cycles, so initial cost is secondary to its long-term performance.
Production: Designed for Efficiency
In contrast, using EDM for production parts typically involves creating specific, complex features that are difficult to machine otherwise. The main concerns are repeatability, cycle time, and cost per part. Efficiency and consistency across a production run are the most critical factors.
| Fokusområde | Tooling Application | Production Part Application |
|---|---|---|
| Primärt mål | Longevity & Durability | Repeatability & Efficiency |
| Material | Härdade verktygsstål | Various Production Metals |
| Nyckelmått | Finish & Detail Accuracy | Cost-Per-Part & Lead Time |
| Volym | Low (Often one-off) | High (Batch or Mass) |
The distinction between EDM tooling vs production parts is crucial for supplier selection. A shop that excels at making single, highly detailed mold cavities may not be equipped for the automation and process control required for high-volume production parts. Their cost structure and expertise are different.
The Supplier’s Perspective
A tooling specialist invests heavily in high-precision sinker EDMs and the expertise to create complex electrodes. They understand how different EDM settings affect the Anisotropisk15 properties of hardened steel, which is critical for preventing premature tool wear and failure. Their quoting process reflects a focus on a single, high-value asset.
On the other hand, a production-focused shop prioritizes wire EDM machines and automated systems. Their strength lies in process optimization to reduce cycle times and ensure every part is identical. They are experts at managing costs over large batches, where a few seconds saved per part translates into significant savings.
Matching the Work to the Shop
Understanding this difference helps you frame your request. When you approach a supplier, clearly stating your application—tooling or production—allows them to provide a relevant quote and proves you know what to look for in a partner.
| Typ av leverantör | Tooling Specialist | Production Specialist |
|---|---|---|
| Expertis | Complex electrode design | Process automation & control |
| Utrustning | High-precision sinker EDM | Automated wire EDM systems |
| Kostnadsmodell | Value-based (longevity) | Volume-based (efficiency) |
| Idealisk projekt | Injection molds, stamping dies | Parts with intricate features |
Knowing whether you need a tool or a production part is the first step. This clarity ensures you engage the right partner, get accurate quotes, and ultimately receive a final product that meets your specific project requirements, whether for longevity or for volume production.
EDM Lead Times — What’s Realistic and What Delays Orders
Setting realistic expectations for EDM machining lead time is crucial. A simple wire EDM part might be completed in a few days, but complex projects can stretch into weeks. Delays are often misunderstood and can lead to frustration if not anticipated.
Key Timeline Factors
Several stages contribute to the overall delivery schedule. The initial setup, machining process, and any required finishing steps all play a significant role. Understanding these elements helps in planning a project schedule more accurately.
Common Influences on Timelines
Here are some typical factors we see that impact lead times for our EDM Machining Services.
| Faktor | Potentiell påverkan |
|---|---|
| Delens komplexitet | Hög |
| Electrode Fabrication | High (for Sinker EDM) |
| Post-Machining Steps | Hög |
| Krav på inspektion | Medelhög till hög |
Understanding the specific causes of delays helps in managing the project timeline. It’s not just about the hours the machine is running; preparatory and finishing work are often the most time-consuming parts of the process.
Deconstructing Common Delays
Electrode Fabrication
For sinker EDM, creating the custom electrode is a project in itself. It requires separate CNC machining, and its complexity can add a week or more to the schedule before the EDM process even starts.
Programming and Setup
Wire EDM requires precise programming paths. Additionally, if the part doesn’t have a pre-existing hole for the wire, drilling a start hole is a necessary preliminary step. These tasks add to the front-end of the EDM machining lead time.
Heat Treatment and Finishing
If a part requires hardening after machining, it must be sent for heat treatment. This process, which can involve Släckning16, often depends on an external vendor’s schedule, adding transit and processing time.
How to Shorten Lead Times
To help us accelerate your order, provide complete and clear drawings from the start. Specifying the required surface finish level and providing a wire start hole can also significantly reduce setup time and streamline the workflow.
Realistic EDM lead times depend on part complexity, electrode needs, and post-machining processes. Clear drawings and specifications are the most effective tools for preventing unexpected delays and ensuring your project stays on schedule with our EDM Machining Services.
EDM for Hardened Steels and Carbide — Where Other Methods Fail
The Post-Hardening Dilemma
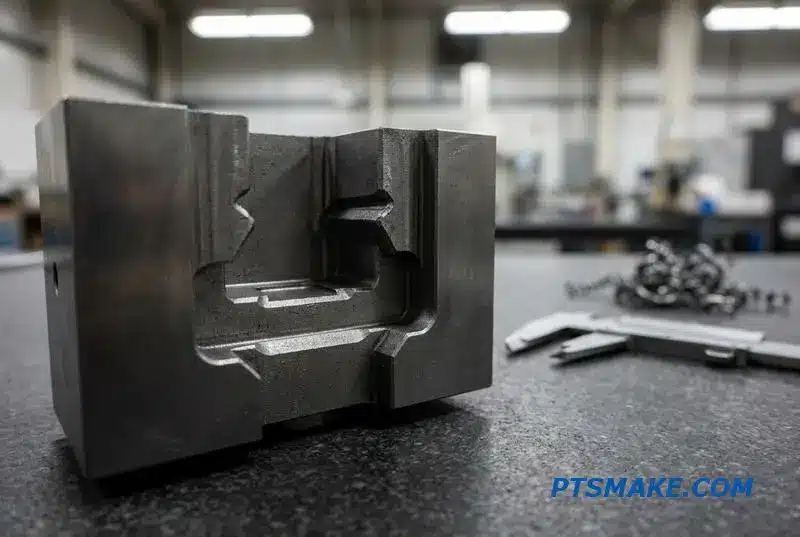
Conventional machining hits a wall with hardened materials. After heat treatment, materials like tool steel or carbide become too tough for standard cutters, which dull or break. This creates a significant manufacturing bottleneck, especially for creating precision features on durable parts.
A Non-Contact Solution
This is precisely where our EDM Machining Services excel. Electrical Discharge Machining is a non-contact process. It uses thermal energy to erode material, completely unaffected by its hardness. This allows us to create intricate features after the material has been fully hardened.
Milling vs. EDM on Hardened Steel
| Funktion | Konventionell fräsning | EDM-bearbetning |
|---|---|---|
| Material Hårdhet | Limited to < 60 HRC | Unaffected by hardness |
| Verktygsslitage | High risk of tool breakage | Electrode wear is predictable |
| Funktionens komplexitet | Limited on hardened parts | Ideal for complex geometry |
The Ideal Manufacturing Workflow
The most efficient process is to machine the bulk of the part while it’s in a softer, annealed state. Once the primary shaping is done, the part undergoes heat treatment to achieve its final hardness. Only then do we use EDM for the final, critical features.
This sequence ensures dimensional stability and prevents the distortion that can occur if complex features are machined before hardening. The process relies on a controlled electrical discharge creating a Plasma channel17 between the electrode and workpiece, melting a tiny portion of the material.
Applications in Die and Mold Making
This method is fundamental in creating punches, dies, and injection molds. For example, we can cut sharp internal corners or intricate cooling channels into hardened tool steel. This makes EDM hardened steel carbide a go-to process for high-wear tooling that requires precision.
Why Supplier Experience is Critical
Working with hardened materials requires specialized knowledge. An experienced supplier like PTSMAKE understands how to manage parameters to prevent micro-cracking and maintain surface integrity. Choosing the wrong partner can lead to premature tool failure, compromising your entire project.
| Faktor | Importance in Hardened Material EDM |
|---|---|
| Inställningar för strömförsörjning | Must be optimized to avoid thermal damage |
| Flushing | Crucial for removing debris and preventing arcing |
| Electrode Material | Copper or graphite selection impacts finish/wear |
EDM is not just an alternative; it’s a strategic advantage for hardened materials. It allows for machining after heat treatment, ensuring final parts have both extreme precision and maximum durability. This capability is essential for high-performance tooling and complex components.
Understanding this fluid’s role is key to grasping how EDM achieves precision without mechanical stress on the workpiece. ↩
Learn how this metallurgical surface alteration can impact your component’s fatigue life and performance. ↩
Understanding electrode wear helps predict final part accuracy and optimize Sinker EDM process parameters. ↩
Understanding this property helps determine if EDM is the right manufacturing process for your material choice. ↩
This principle explains how EDM removes material non-mechanically, which is key to its precision and versatility. ↩
Learn how this thermally altered region impacts your part’s mechanical strength and fatigue life. ↩
Understanding this ratio is key to designing effective deep features for cooling, venting, and other functional applications. ↩
Understand how machining choices impact a material’s final properties and long-term durability in demanding applications. ↩
Understand how this material property can impact subsequent machining and part performance. ↩
Learn how this property impacts part performance and reliability in high-stress applications. ↩
Understanding this effect helps prevent premature part failure and improves material integrity. ↩
Learn how this principle affects material stability and precision in advanced manufacturing applications. ↩
Explore how this key metric influences project timelines and costs in manufacturing. ↩
Explore the science of measurement to understand how precision and accuracy are scientifically guaranteed in manufacturing. ↩
Understanding this property helps predict tool wear and ensures the longevity of molds and dies. ↩
Learn how this rapid cooling technique modifies metal microstructures for desired hardness and durability. ↩
Understanding this concept explains the physics behind EDM’s unique material removal capabilities. ↩