
Plastic CNC Machining Services
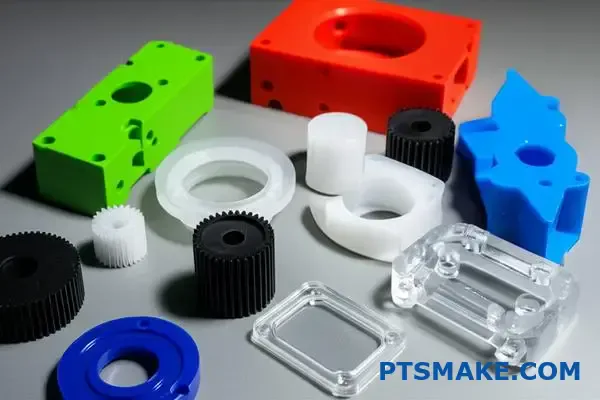
Custom plastic parts, made to your drawings. From a clear cover to a complex housing, PTSMAKE combines CNC machining with material selection, stress relief and clear polishing.
Get a Plastic Machining QuoteShare your CAD model, material and quantity to get started.
- Dimensional Tolerances
- ±0.05 mm
- Materials
- 16 Options
- Order Quantities
- Prototype to Production
- Additional Processing
- Annealing & Clear Polishing
Material, geometry and inspection requirements confirmed during drawing review.
Engineering plastics, high-performance polymers and insulating laminates.
Machining routes matched to the part and the order.
Available where the material and part require it.
Why Choose PTSMAKE for Your Plastic Parts?
The right resin, a stable part and the required surface finish belong in the same machining plan. We help you bring those decisions together before production.
Material Selection for the Job
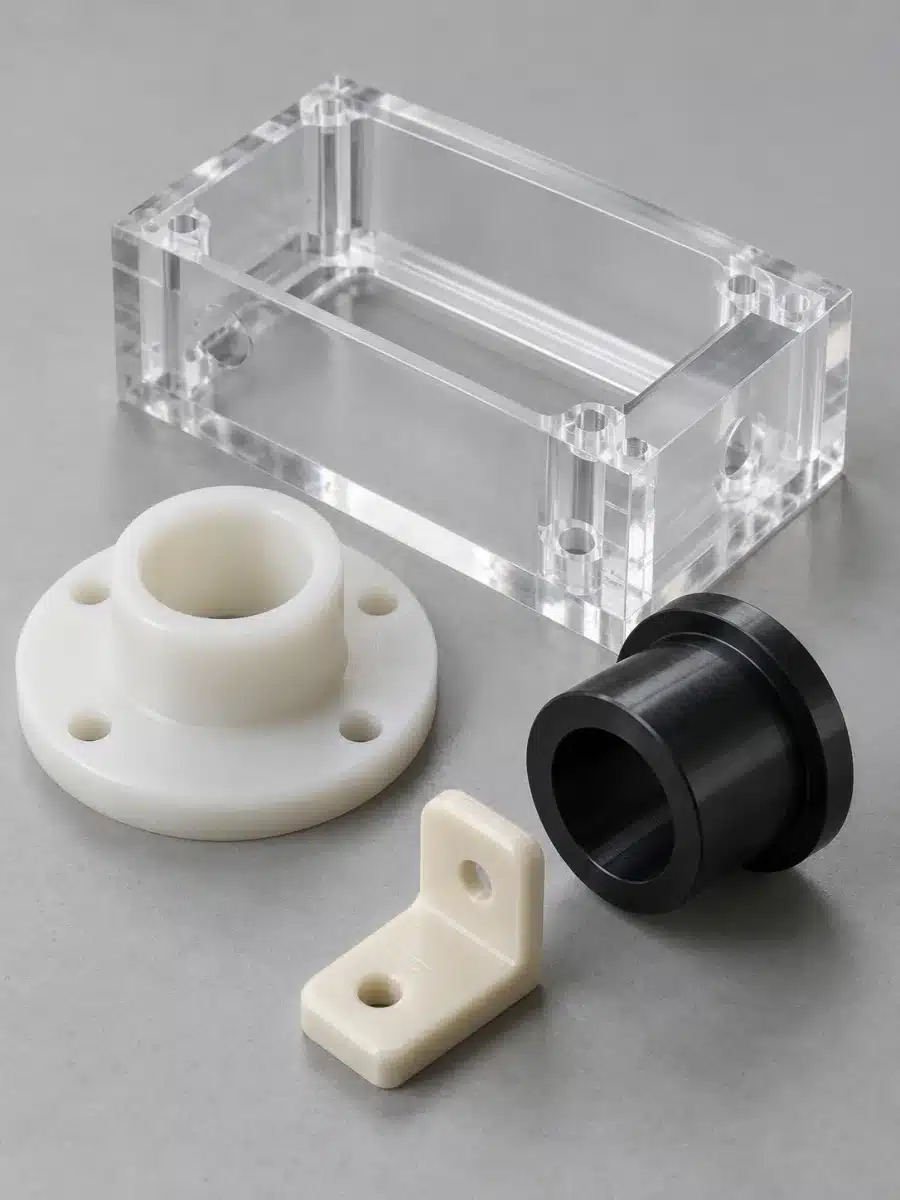
Choose materials around the loads, temperature, chemicals and appearance your part will face. We work with common engineering plastics, high-performance polymers and glass-epoxy laminates.
Clear Surfaces Where They Matter
Clear polishing is available for suitable transparent plastics. Mark the viewing surfaces on your drawing so the polishing method, edge condition and desired appearance can be agreed together.
Stress Relief for Stable Dimensions
We provide stress-relief annealing when the material and part require it. Planning this step alongside roughing and finishing helps manage the movement that can follow heavy material removal.
Plastic Machining Capabilities
Match the process to the shape. From flat panels to multi-face housings and turned components, PTSMAKE machines plastic parts to your drawings and specifications.
CNC Routing
Profile plastic sheet into panels, guards, covers and flat components. Hole locations, edge quality and sheet flatness are reviewed together, especially when the part must fit a larger assembly.
Discuss a Routed Part3/4/5-Axis CNC Milling
Machine pockets, channels, mounting faces and features on multiple sides. Milling is suited to plastic manifolds, housings and fixtures whose dimensions must relate accurately to one another.
Discuss a Milled PartCNC Turning and Swiss Machining
Produce round parts with concentric bores, shoulders, grooves and threads. We choose between conventional turning and Swiss machining based on the component’s proportions, features and order quantity.
Discuss a Turned Part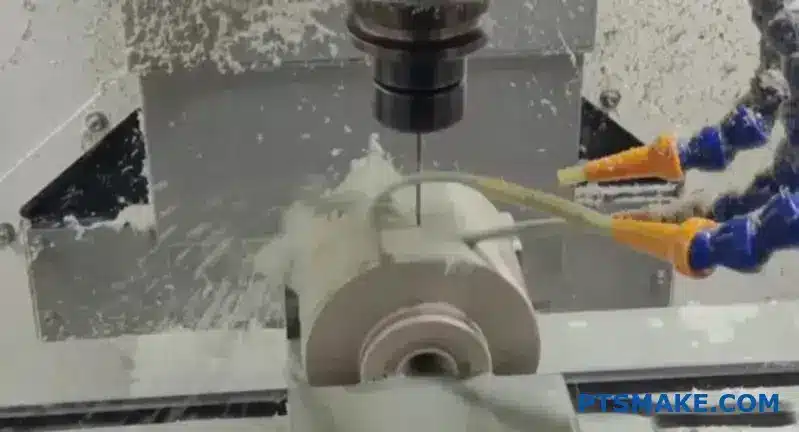
Plastic Materials for CNC Machining
Explore 16 material options. Start with the working environment and the function of the part, then specify the grade, fillers and stock requirements for your quotation.
POM (Acetal)
Gears, bushings, locating parts
Machining & Specification
Acetal combines stiffness, low moisture uptake, and favorable sliding behavior for gears, bushings, and locating parts. POM-C and POM-H have different property profiles; specify the required type or exact grade when fit, wear, or chemical exposure drives selection.
Machining consideration: Sharp tools and balanced stock removal help control heat and movement around close-fitting machined features.
- Design Priority
- Stable fits and sliding contact
- Specify
- POM-C or POM-H; exact grade
ABS
Housings, handles, prototypes
Machining & Specification
ABS is a useful choice for housings, handles, and functional prototypes that need impact toughness and straightforward machining. Its balance of stiffness and toughness varies by grade, so match the stock material to the intended service conditions.
Machining consideration: Support thin walls and control cutting heat to limit deflection and preserve the finished shape.
- Design Priority
- Impact toughness and machinability
- Specify
- Grade, color, service conditions
Nylon (PA6 / PA66)
Bushings, rollers, wear parts
Machining & Specification
Nylon offers toughness, wear resistance, and useful sliding properties for bushings, rollers, and mechanical components. PA6 and PA66 are distinct choices. Both absorb moisture, which can change dimensions and stiffness, making the operating environment important for fitted parts.
Machining consideration: Agree on moisture conditioning and inspection conditions before assigning tolerances to critical bores and fits.
- Design Priority
- Toughness and wear resistance
- Specify
- PA6 or PA66; moisture conditions
PET
Guides, rollers, fitted components
Machining & Specification
Semicrystalline PET stock combines stiffness, low moisture uptake, and useful wear behavior for guides, rollers, and fitted components. These machining grades differ from amorphous packaging PET. Check hot-water and chemical exposure against the selected grade before choosing it.
Machining consideration: Confirm the machining stock grade; do not substitute transparent packaging sheet based on the abbreviation.
- Design Priority
- Dimensional stability and wear behavior
- Specify
- Semicrystalline stock grade; service media
PVC
Insulators and chemical-contact components
Machining & Specification
Rigid PVC is an option for machined components that need chemical resistance and electrical insulation. Specify unplasticized PVC when rigidity matters; flexible PVC is a different formulation. Chemical compatibility depends on the fluid, concentration, and operating temperature.
Machining consideration: Control cutting heat and support the workpiece; confirm the rigid stock grade before planning machining.
- Design Priority
- Rigidity and chemical compatibility
- Specify
- Rigid PVC grade and service media
PEEK
Bushings, rings, loaded components
Machining & Specification
PEEK is considered for loaded components exposed to heat, wear, or demanding chemical environments. Unfilled and reinforced grades serve different needs. Choose the grade around actual loads, mating surfaces, and chemical exposure before finalizing the part specification.
Machining consideration: Identify fillers before machining; reinforcement affects tool wear, surface finish, and the behavior of fits.
- Design Priority
- Heat, wear, and chemical exposure
- Specify
- Exact grade, fillers, operating conditions
PEI
Insulating components and rigid supports
Machining & Specification
PEI combines stiffness, heat resistance, and electrical insulation for components that must retain their shape in demanding service. Natural unfilled grades are typically translucent amber. Reinforcement changes the property balance, so specify the grade rather than relying on appearance.
Machining consideration: Review cutting fluids and residual stress; some solvents can trigger cracking in stressed PEI components.
- Design Priority
- Electrical insulation and heat resistance
- Specify
- Exact grade, fillers, chemical exposure
PAI
Bearings, seals, loaded components
Machining & Specification
PAI is considered for demanding bearings, seals, and loaded components where heat and wear challenge other polymers. Structural and wear grades are not interchangeable. Moisture absorption can affect dimensions, so material condition belongs in the specification for precision parts.
Machining consideration: Confirm the supplied material condition and moisture state before setting machining allowances and final inspection.
- Design Priority
- Load retention and wear performance
- Specify
- Exact grade and moisture condition
PTFE
Seals, bushings, chemical-contact parts
Machining & Specification
PTFE suits seals, low-friction interfaces, and components exposed to chemicals that would challenge many other plastics. Its relatively low stiffness and substantial thermal expansion require careful fit design. Filled grades change performance, so the compound must be specified.
Machining consideration: Use gentle workholding and evaluate dimensions at an agreed temperature, especially for thin sealing features.
- Design Priority
- Chemical compatibility and low friction
- Specify
- Virgin or filled grade; service media
PMMA (Acrylic)
Viewing windows, covers, visual prototypes
Machining & Specification
Acrylic is a candidate for transparent covers, viewing windows, and visual prototypes. Machining leaves visible tool marks, so clarity requirements should identify which faces need polishing. Cast and extruded stock behave differently during processing and should be specified.
Machining consideration: Protect edges from chipping and control polishing heat; define visible surfaces before choosing the finish.
- Design Priority
- Transparency and appearance
- Specify
- Cast or extruded; polished faces
PC (Polycarbonate)
Viewing components and protective covers
Machining & Specification
Polycarbonate is a candidate for transparent covers and viewing components where impact toughness matters. Machined surfaces may need polishing to achieve the required clarity. Review exposure to cleaners and solvents, since chemical compatibility can limit an otherwise suitable design.
Machining consideration: Specify transparent viewing faces and check fluid compatibility before machining or polishing stressed, detailed features.
- Design Priority
- Transparency with impact toughness
- Specify
- Grade, clarity, cleaners and solvents
HDPE
Spacers, supports, wet-environment parts
Machining & Specification
High-density polyethylene is a lightweight option for machined components exposed to moisture and compatible chemicals. It offers low water uptake and can be machined from plate or rod. Account for stiffness and thermal expansion when designing close fits.
Machining consideration: Support broad faces and limit clamping pressure to avoid distorting the part during final cuts.
- Design Priority
- Low water uptake and chemical resistance
- Specify
- HDPE grade, loads, service temperature
UHMW-PE
Guides, liners, wear strips
Machining & Specification
Ultra-high-molecular-weight polyethylene is used for guides, liners, and wear strips that benefit from low friction and impact toughness. It belongs to the PE family. Thermal expansion and part flexibility need attention when long components include mounting holes or close fits.
Machining consideration: Support long sections during machining and allow for temperature-driven movement when locating holes and fits.
- Design Priority
- Low friction and abrasion resistance
- Specify
- Grade, mounting method, service temperature
PE (Polyethylene)
Guides, liners, general components
Machining & Specification
Polyethylene is a material family that includes HDPE and UHMW-PE, with grades offering different stiffness and wear behavior. A drawing marked only PE leaves an important choice open. Identify the subtype and operating conditions before comparing machining quotes.
Machining consideration: Resolve the PE subtype first; machining allowances and fit expectations depend on the selected stock.
- Design Priority
- Match the polyethylene subtype
- Specify
- PE subtype, grade, operating conditions
FR4
Insulating plates, spacers, rigid supports
Machining & Specification
FR4 is a glass-fabric-reinforced epoxy laminate used for electrical insulation and rigid components. Its flame-retardant grade designation distinguishes it from standard G-10. Specify the required laminate and finished-part requirements; a material designation alone does not certify an assembly.
Machining consideration: Plan for abrasive glass fibers, support drilled exits, and inspect cut edges for laminate damage.
- Design Priority
- Insulation with a flame-retardant laminate
- Specify
- Laminate grade, thickness, electrical requirements
G-10
Insulating spacers and structural plates
Machining & Specification
G-10 is a glass-fabric-reinforced epoxy laminate for rigid insulating and structural components. Its layered construction affects machining and load direction. Do not assume it has FR4's flame-retardant specification; identify the required laminate grade directly on the drawing.
Machining consideration: Consider laminate direction, use suitable tooling, and support holes to reduce chipping at tool exit.
- Design Priority
- Rigidity and electrical insulation
- Specify
- Laminate grade and loading direction
Need another plastic, a filled grade or a specific material brand?
Ask About Other MaterialsMaterial descriptions are selection guidance, not grade-specific design data. Confirm the exact resin and its supplier data sheet before setting performance requirements. POM, PEI, PTFE and PAI also include branded grades; a brand name must be specified when it is required.
Design Guidelines for Plastic CNC Machining
Keep the features that matter to function. Simplify the details that add machining time, deflection or unnecessary inspection work.
Keep Walls Consistent
Thin plastic walls can flex during machining and move after unclamping. Use consistent sections where possible, and review long unsupported walls before setting the final thickness.
Why It Matters
A stable section is easier to hold and finish. Keep the thickness needed for function instead of applying one minimum to every resin.
Give Internal Corners a Radius
A rotating cutter leaves a radius in an internal corner. Make that radius generous enough for the pocket depth, and use consistent radii where they do not interfere with the mating part.
Why It Matters
Larger, accessible corner radii can reduce tool changes and long, slender cutters. A relief feature may solve a square mating-part requirement.
Make Holes Accessible
Deep, narrow holes increase the difficulty of removing chips and controlling heat. Keep holes only as deep as the function requires, and identify any bore that locates a shaft, seal or fastener.
Why It Matters
A through-hole may be simpler than a deep blind hole when the design permits it. Do not change a sealing or structural feature just to simplify machining.
Tighten Only the Functional Dimensions
Put close tolerances on the features that control assembly or performance. Plastic dimensions can change with temperature and moisture, so define the inspection conditions when the fit depends on them.
Why It Matters
Separating functional dimensions from general features helps focus machining and inspection effort where it improves the part.
Support Slender Features
Tall ribs and slender projections may deflect under cutting or clamping forces. Where the function permits, shorten unsupported lengths, add support and avoid abrupt changes at the base.
Why It Matters
A supported feature is less likely to vibrate during finishing. Preserve the intended flexibility when a tab or spring feature must bend in use.
Plan Threads Around Repeated Assembly
Specify thread size, depth and access. For frequently assembled joints, consider whether a metal insert is appropriate for the resin, surrounding wall thickness and required pull-out resistance.
Why It Matters
An insert can protect a repeatedly used joint, but it also needs an installation method and enough supporting material. Direct plastic threads can suit other applications.
Reduce Unnecessary Setups
Group accessible features where possible and give important dimensions a clear datum structure. Features on several faces may require additional setups or a different machine configuration.
Why It Matters
Fewer setups can shorten handling time and simplify control of related dimensions. Preserve the geometry required by the assembly before optimizing the machining route.
What Is Plastic CNC Machining?
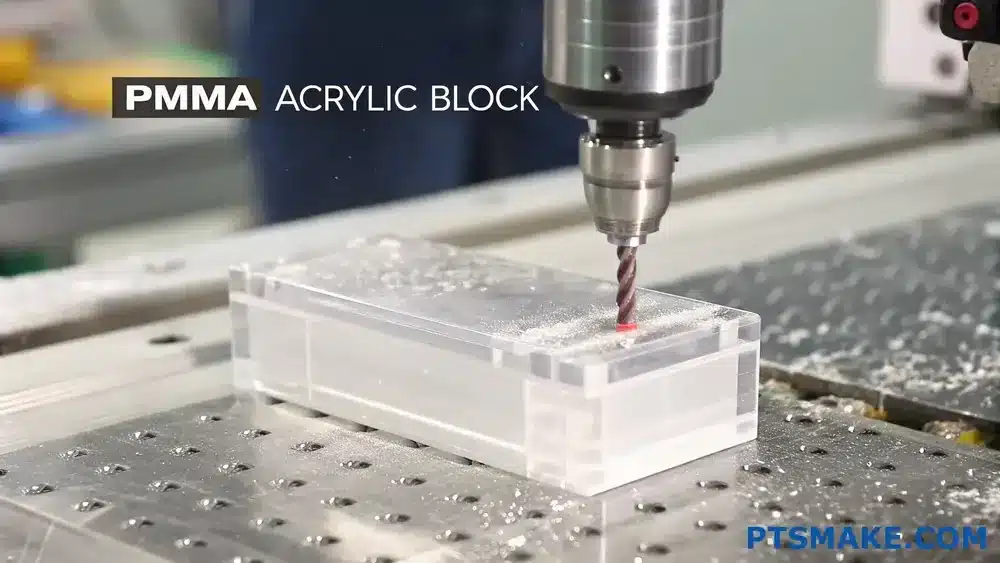
CNC machining removes material from solid plastic stock to create a part from a digital model. A mill cuts pockets and external shapes, a lathe produces round features, and a router cuts profiles and openings in sheet.
This route uses stock material rather than a mold. It suits functional prototypes, replacement parts and production components when the required resin is available in a machinable form.
The drawing remains essential: a CAD model describes shape, but does not always define critical fits, datum references, threads, surface appearance or inspection conditions. Supply both when these details determine whether the part will work.
For plastic parts, the finished dimensions also depend on temperature, moisture, clamping and residual stress. Material selection and the machining sequence need to account for these effects, particularly on thin walls and close-fitting assemblies.
Back to contents ↑Plastic Part Examples
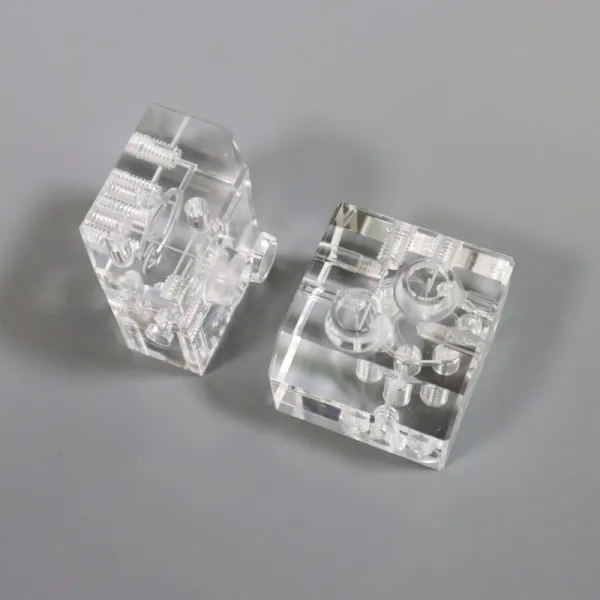
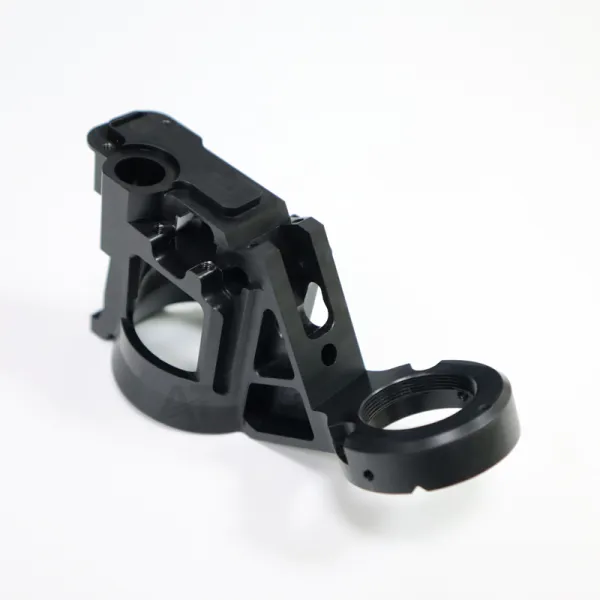
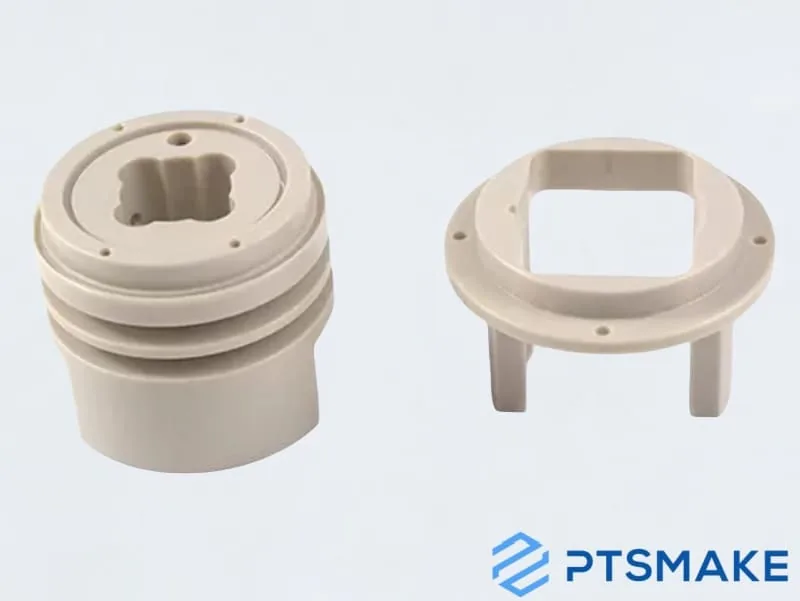
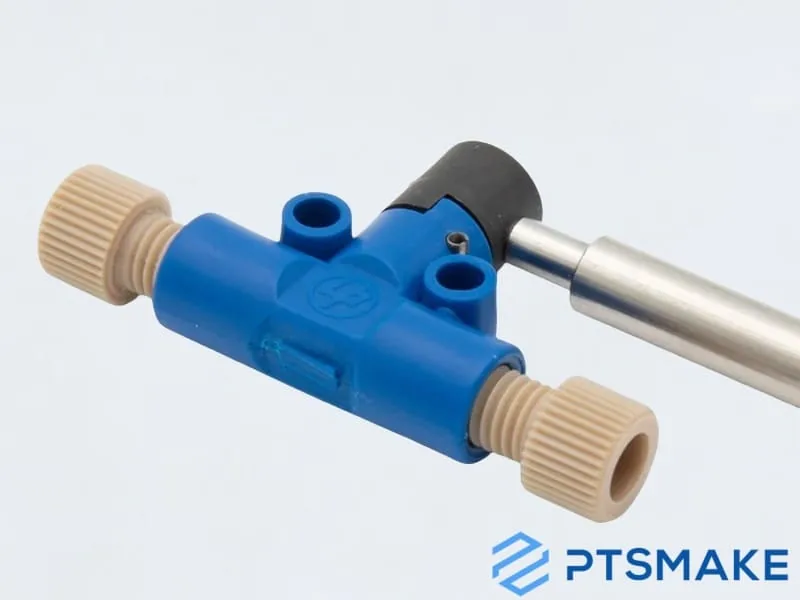
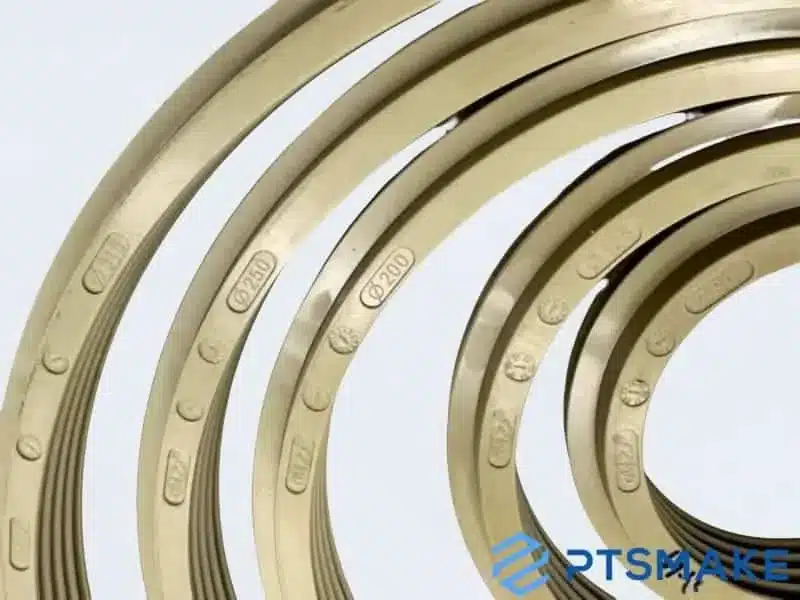
Explore the shapes that machining can produce: clear housings, threaded parts, detailed manifolds and components with features on several faces.
Use these geometries as a starting point for discussing your own design. Your drawing defines the material, dimensions and finish of the parts you order.
Discuss Your Part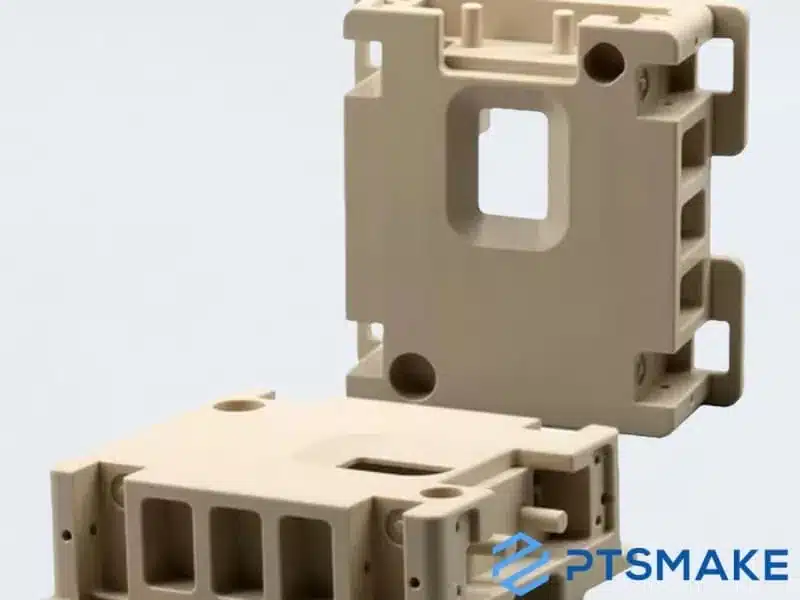
Advantages of CNC Plastic Machining
A flexible route when you need useful parts from solid plastic stock.
No Dedicated Mold
Start from a CAD model and drawing without committing to a production mold. This can suit early functional parts, design revisions and quantities that would be difficult to justify with dedicated tooling.
Control the Functional Features
Machine the bores, faces and locating details that make the part work in an assembly. The drawing can distinguish critical dimensions from features that allow a wider tolerance.
Choose From Solid Stock
Select a machinable rod, sheet or plate in the required polymer. The range includes everyday plastics, high-performance resins and insulating laminates, each with its own processing and design considerations.
When to Choose CNC Machining Over 3D Printing
Choose the process around the finished part. CNC machining and 3D printing solve different design problems; neither is the best choice for every geometry or quantity.
You Need a Particular Stock Material
Machining can be a good fit when the specified resin is available as rod, plate or sheet. Match the exact grade and filler content to the application. A printable material with a similar name may have different properties, processing history or available documentation.
Fits and Mating Surfaces Matter
Choose CNC when bores, sealing faces or locating features need controlled dimensions and accessible machined surfaces. Highlight those features on the drawing. Printing may still be useful for early fit checks, or combined with machining where the design supports both processes.
Appearance Is Part of the Function
Machining and suitable polishing can support transparent viewing areas or a defined surface finish. Specify the surfaces that will be seen and those that must maintain a fit. Clarity alone does not define optical performance, haze limits or an acceptable cosmetic standard.
The Geometry Suits Tool Access
Open pockets, external contours and accessible holes often suit machining. Enclosed internal channels or shapes that trap a cutting tool may favor printing or a split assembly. Compare the complete route, including finishing, setup time and waste, rather than assuming one process is always cheaper.
Applications for Machined Plastic Parts
Plastic components can provide electrical insulation, wear resistance, lower weight or transparency. Suitability depends on the grade and the conditions in which the part will be used.
Semiconductor Equipment
Insulators, fixtures and handling components can benefit from engineered polymers. Define chemical exposure, temperature and any cleanliness or electrical requirements before selecting the grade.
Automotive and Aerospace
Machined polymers can serve in lightweight brackets, bushings and electrical components. Specify the operating loads and environment; an industry application does not itself establish a material approval.
Food and Packaging Equipment
Guides, wear strips and equipment parts need materials suited to their cleaning regime and operating conditions. Where food contact applies, identify the required grade and documentation explicitly.
Medical and Laboratory Equipment
Housings, instrument components and fixtures may need transparency or chemical resistance. Discuss cleaning, sterilization and documentation requirements separately; medical use is not an automatic biocompatibility claim.
From Your Drawing to Plastic Parts
Send PTSMAKE your CAD model, dimensioned drawing, material grade and quantity. Identify critical fits, visible surfaces and the date you need the parts so the quotation reflects the complete job.
Production Lead Times
Final lead time is confirmed with your quote, based on the part, material, quantity, finishing and inspection requirements.
Frequently Asked Questions
Practical details for your plastic machining order.
What Do You Need to Quote a Plastic Part?
Send a CAD model and dimensioned drawing, the required plastic grade, quantity and target date. Mark critical dimensions, threads and visible surfaces. Include any material documentation or inspection requirements. If the material is undecided, describe the operating loads, temperature and chemical exposure, along with the required appearance.
What Tolerance Can PTSMAKE Hold on Plastic Parts?
We offer dimensional tolerances of ±0.05 mm for plastic machining, with feasibility confirmed against the material and drawing. Thin walls, long features and moisture-sensitive resins can need particular attention. Identify the dimensions that control fit and specify any required measurement temperature or conditioning so the inspection basis is clear.
Do You Offer Stress-Relief Annealing?
Yes. PTSMAKE can provide stress-relief annealing as part of the plastic machining route. Whether it is needed, and where it belongs in the sequence, depends on the resin, stock condition, geometry and amount of material removed. It helps manage residual stress; it is not a guarantee against movement under every service condition.
Can You Polish Transparent Plastic Parts?
Yes. Clear polishing is available for suitable transparent plastics. Tell us which faces must be transparent, which dimensions must be protected and what appearance you expect. A visual reference or agreed sample helps define the result. Optical performance requirements need a separate specification rather than a general request for a clear finish.
How Is the Machining Price Calculated?
The quote depends on material and stock size, quantity, machining time, setups, tolerances, finishing and inspection. Deep pockets, difficult tool access and tight requirements on nonfunctional surfaces can increase the work involved. We can discuss design changes, but changes to a drawing need your agreement before manufacture.
Can I Order Prototypes and Production Quantities?
Yes. PTSMAKE supports plastic prototypes, small batches and production runs. Include your initial quantity and expected repeat demand when requesting a quote. The production lead times above provide the planning ranges; the schedule for your specific material, part and finishing requirements is confirmed with the quotation.
Can You Supply Another Material or Surface Finish?
Send the exact material grade or finish specification with your drawing. The options on this page are a starting point. Filled materials, branded grades and additional finishes need review for availability and compatibility with the part. We will confirm the agreed specification in the quotation rather than substitute a material without discussion.
Ready to Machine Your Plastic Parts?
Share your drawing and requirements. We’ll help you settle the material, machining route and finish.
Get a Plastic Machining Quote